#Extruders General Chatter
2055 messages · Page 3 of 3 (latest)
 rugged yew
i just looked this is the extruder motor i have
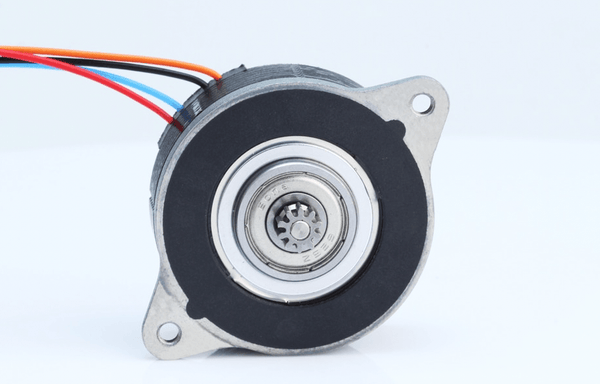
West3D 3D Printing Supplies
This is the pancake motor used on the V01 mini-afterburner and Stealthburner. This is a genuine Moons' Motor sourced by TriangleLab and used in the Orbiter, Sherpa and other extruders.
 deft galleon
rugged yew
i just looked this is the extruder motor i have
https://west3d.com/products/moo...
That's an excellent motor and can withstand increases in run_current. However, that should not be needed. If you seeing motor skipping, I'd check that any grub screws in the gearing are tight, then make sure the tensioner arm is not too tight, it should be just tight enough that it feeds the filament through, but not so tight the filament gets ground. To achieve higher flow, as thunderkeys said, I'd increase your PLA temp by 10C at a time, but keep it only up to around 260C. With PLA, the higher the flow, the hotter the nozzle needs to be.
rugged yew
deft galleon
That's an excellent motor and can withstand increases in run_current. However, t...
idga set so no grub screws, i tightened the tension arm so that it has full engagement of the square nut but no more. i may have to find a way to back that off. i dont believe its grinding filament though. ill play with it wheni get a chance
deft galleon
rugged yew
idga set so no grub screws, i tightened the tension arm so that it has full enga...
Best way is to feed filament through the extruder and then pull it back out. There should be slight indents in it. If it's too smooth, it needs more. If the teeth are getting right into the filament, it's probably too much
rugged yew
i verifyed its not grinding filament but it is leaving deep indents in petg right now, my thumb screw has a 12mm spring that gets compressed down to 7 when its threaded for only full engagment of the sqare nut

going to sweep 15-40 mm^3/s at 220 with pla, with a longer screw instead of the thumb knob to reduce tension
deft galleon
rugged yew
going to sweep 15-40 mm^3/s at 220 with pla, with a longer screw instead of the ...
I do think you may struggle at 220C. PLA likes to heat creep up the hotend and having the temp low usually ends with a clog and could be what you are seeing. If you do have problems at 220, try 230 and then 240 to see if it helps
rugged yew
deft galleon
I do think you may struggle at 220C. PLA likes to heat creep up the hotend and h...
im just checking to see if lower tension helps, if i get above what i did before ill increase temps.
 mellow cradle
@glossy sentinel might also be able to chime in on his experience with pika and PLA
rugged yew
i dont print with pla often i just want to tinker with it before i blow through my abs
i dont need the full 40-50mm^3/s 25 just seems underwhelming
mellow cradle
PLA is underwhelming.
rugged yew
thats fair i may just send it with abs after this
 glossy sentinel
What brand of material is this
glossy sentinel
Ok, 25 defs seems low. Guessing 0.4? 220 might be low for their material, is your door open while printing?
rugged yew
0.4 they call for 215, the door is open. i ran the test at 240 i still have to look at it
glossy sentinel
For reference our flow with Jesse PLA at 230 is about 30 cubic on an x1c, that extruder is stronger so should do better
rugged yew
at 240 it looks like i get to around 30 cubic when i start to see issues
glossy sentinel
Correction 41 cubic, misread my spreadsheet. Just checking but it isnt a PLA Pro or plus or anything like that. Ive printed Polars PHA just not super familiar with the PLAs
rugged yew
thats just when it thins out i dont get holes/gaps until 35
normal pla, i think its litterly just pla and colorant
glossy sentinel
Alright
rugged yew
I measured up until the red line, that's where it starts to get artifacts, but it has an even shein across the whole test and the upper layers where there's gaps aren't brittle
 glossy sentinel
The sheen tells me that the extruder is likely giving up before you run out of melt
Perhaps the motor is losing torque at fast RPM
rugged yew
the other thing that makes me think that is with cw2 it would click and pop, now it just stalls
the only other thing would be the pla creeping and jamming up on the cold side of the hot end
i think im going to run some abs and see what happens
 warm hare
I built a WWBMG yesterday and got a few prints out of it that looked good, then came back to a ‘failed’ print this morning and I think I had the tension arm set too tight. The filament was ‘pigtailed’ like this from the extruder gears to the top of the heatsink

I’ve cleared the extruder but need to disassemble my hotend so I can heat gun the heatsink
 wintry dew
warm hare
Umm, are you missing a section of PTFE tube. I don’t see how it could pigtail like that unless there was space for it to escape.
And that looks very close to 4mm OD.
warm hare
Dang, I was wondering if I needed PTFE in there but neither the A4T or WWBMG guide I was looking at mentioned it. Makes a ton of sense though!
Wish me luck at somehow getting this out
rugged yew
i think its assumed to be part of the "hot end assembly" sense it varys on hot end
warm hare
Alright I had Sunday morning brain but after cutting the ptfe three times I have the right length, thanks for the help!
 pastel arrow
Are there any extruders that have filament sensors before and after the gears to make filament loading easier?
 delicate charm
I know that the A4T version of the WWBMG has dual sensors
https://github.com/Armchair-Heavy-Industries/A4T/tree/main/STL/WW-BMG for A4T
GitHub
[A]nother [4]010 [T]oolhead. A toolhead for Voron front rail printers built around 4010 blower fans, efficient ducts, and easy assembly. - Armchair-Heavy-Industries/A4T
 uncut mountain
Hello Everyone. I have been using for some time now a Nebula Extruder and even though i can say its very good with PLA, PETG and ABS i can seem to make the lever work 100% properly with PA6 GF or any sort of TPU. Does anyone have an actual cad of the case to make a redesign and some minor path changes along with a proper lever?
deft galleon
uncut mountain
Hello Everyone. I have been using for some time now a Nebula Extruder and even t...
It's on BTT's Github: https://github.com/bigtreetech/Nebula/tree/master/3D Model/Reference Cad Model
I don't know whether that's complete CAD or just for reference. You could have a look on grabcad.com as well
uncut mountain
deft galleon
I don't know whether that's complete CAD or just for reference. You could have a...
It's reference. Looking for something I can optimize filament path and constraints as also change the lever and spring from the tiny screw that within half a turn it's either fully loose or very tight
 dry fossil
Generally speaking, what is a minimum ratio we shouldn't dip below for an extruder? HGX-Lite is something like 9.58:1. is 5:1 too much?
And is the ratio more about precision, or torque?
 pine sun
dry fossil
Generally speaking, what is a minimum ratio we shouldn't dip below for an extrud...
5:1 is perfectly fine it's the standard cw2 ratio. 50t BMG gear and 10t motor
The higher the ratio the more torque you have
I don't really think it's about precision
 rigid vale
 hmm but with a too large a gear reduction the stepper must spin very fast
and steppers lose a lot of torque at speed
pine sun
rigid vale
<:thunk:837326825364914206> hmm but with a too large a gear reduction the steppe...
Yes that's correct 👍
 queen skiff
uncut mountain
It's reference. Looking for something I can optimize filament path and constrain...
I looked into the nebula a while ago, looked like an hgx with an inlet switch and a planetary instead of traditional gear reduction.
I have just the thing for you, an LGX re-case. It really only has two positions, fully tight or loose. The middle position is not useful yet (or never). For full on/off, you can just leave out the middle ball spring. Next time I pull it apart, I will do just that. All step files have been provided. I have put an unreasonable amount of time into them. The HGX or LGX spring conversion would be very similar to that setup, but the LGX lever is pretty cool I was thinking of putting a cam lever on the spring version, but I am a bit burnt out from this project. It is done for now, it will just get minor updates.
https://discordapp.com/channels/460117602945990666/1551623361560445050
 wraith viper
Hey all, I'm trying to fit an hgx lite onto an a4t with ebb36. Does anyone have any experience with this combo?
 ruby pumice
wraith viper
Hey all, I'm trying to fit an hgx lite onto an a4t with ebb36. Does anyone have ...
Probably best to ask on annex where A4T lives
queen skiff
uncut mountain
It's reference. Looking for something I can optimize filament path and constrain...
I have a solution for you. it is almost universal. A cam nut. I find that no spring is needed, but can always print a tpu washer if the lever itself does not have the spring required. This one was from parts from a real one, but the center can be found online searching for dowel nut or barrel nut or quick release.

 glad onyx
What extruder should I use on my stealth burner?
Are there any with integrated filament movement detectors like the roadrunner?
 warped totem
glad onyx
Are there any with integrated filament movement detectors like the roadrunner?
Check in #multimaterial_and_u but it seems that toolhead sensors are no longer needed for filament changers. As far as runout goes, by the time it gets to your toolhead, it’s probably too late to pause the print.