Why does it "feel like a kids toy", the thing was in the mail today. Yet to try, but it grabs the filament good and seems to run smooth. Metal frame, gears are a mix of plastic and metal. I am confident the thing will work. (I will report, should I ever get it on the machine).
Few days ago I changed the idler gear on the "mini stealth burner" (I think this is how its called). A plain 8.3 mm cylinder with the 9.5 mm 17 tooth gear, this works much better already than two serrated grooves.
#Extruders General Chatter
1991 messages · Page 2 of 2 (latest)
 blissful barn
The issue is that the cylinder section of those gears was probably too small; at the same time the grooves too deep. As a result the squish of the plastic was not good enough. I could pull the filament through without driving the motor back. One groove removed improves it (not exactly the point of the two gear system :-), but it works better without the 2nd groove).
At some point the gears bottom out then the distance on the grooved side cannot become smaller anymore.
 untold ivy
I use HGX extruder gears
They work great. And there are many different prints for them
untold ivy
blissful barn
The issue is that the cylinder section of those gears was probably too small; at...
This is usually a print issue. You may have to reprint your parts and check tolerances. Printer must be calibrated
blissful barn
untold ivy
This is usually a print issue. You may have to reprint your parts and check tole...
No it is not a print issue. The driven gears cannot get closer to each other, than the pitch circle radius of the two gears. Here 0.5x17x2=17mm. :-). If the "filament transport knurled drums" are smaller than 7.6 mm there will be no grip on the filament.
untold ivy
blissful barn
No it is not a print issue. The driven gears cannot get closer to each other, th...
Yes this is a print issue you need to reprint the parts
You really have to make sure you printer is calibrated before you print these parts
blissful barn
untold ivy
Yes this is a print issue you need to reprint the parts
The gears are not printed.
untold ivy
blissful barn
The gears are not printed.
Its not the gears it's the part that holds the gears
blissful barn
untold ivy
Its not the gears it's the part that holds the gears
Nope!
blissful barn
I try to make a sketch to explain.
untold ivy
I understand what you are saying..
Its fairly common for cw2 if you printer isn't calibrated correctly
For the filament to slip
And not get grip
blissful barn
When the gears botton out on the teeth (my calculation above is wrong, 4am...). And the cylinders are too small, the filament can slip. There is still "movement" in the plastic parts, but the gears are in their closest possible position.
I checked bondtech clone gears from another source and they have a more shallow groove & bigger cylindrical part. Yes: after messing about with the gears I calibrated completely new.

 blissful barn
What I did: replaced the idler with a "no groove variant" and recalibrated. (at least it seems to work, without having researched to the bitter end) Calibration was repeatable and prints finish, without "air printing".


 icy orbit
Does anyone know of a lightweight extruder that has a latch like clockwork 2 ?
The actual Sherpa, Orbiter etc need 2 hands to load filament (one pressing the arm and another pushing the filament inside)
Sherpa Mini with a latch would be neat.
 deft flame
I'm trying to understand the pros and cons of Orbiter 2.5 vs Galileo 2. I understand it's single and dual gear, and more or less understand the differences, but I'm not familiar with the specifics here. Why would I choose one or the other? (Undecided on hotend but will be a stealth changer so might be different ones.)
 ruby pumice
deft flame
I'm trying to understand the pros and cons of Orbiter 2.5 vs Galileo 2. I unders...
Which toolhead do you plan to use on the SC?
deft flame
ruby pumice
Which toolhead do you plan to use on the SC?
Yavoth
ruby pumice
deft flame
Yavoth
I think it is hard for most of us to testify which is better, I believe the Orbiter can produce more push force for obvious reasons. I run both and judgement is still out.
So probably most important is which format you like. Orbiter is pre-built and generally not rebuilt into anything. Whereas G2 can go into SB as G2E or on top of most other toolheads as either G2SA or WWG2. I'm planning to do SC with WWG2s on top myself.
If I were you, I'd evaluate my toolhead filament sensing needs before deciding too.
Also prob better to ask on the tool changer discords as they may have more sage advice
deft flame
ruby pumice
I think it is hard for most of us to testify which is better, I believe the Orbi...
There was a conversation yesterday on the SC discord, but nothing really pointing a direction there. Different people had different ones and liked them but none really could compare a reason to choose one over another either so I thought the extruders discord might have more sage advice, haha
I've found I can get sherpa mini the cheapest. O2 and G2 about the same price, so there's that
ruby pumice
If you are building a SC, cost is not a consideration 
Yeah, other extruders are slightly cheaper, especially when you multiply by number of toolheads. But I calculated it, not MUCH cheaper, since G2 and Orb both contain the motor too.
Up to the builder though, not sure you want to build such an expensive printer and put the cheapest possible extruder on it
deft flame
Yeah, it's not necessarily about cheapest possible, but if there's no disadvantage, why not (the more tools the more it matters.) A few similar convo heads have me thinking of upgrading to the less cheap shperpa with bondtech gears....if I'm going that route, maybe getting 3 sherpas and 3 g2's is the way to go since I can't seem to decide and they're the same price.
 thorny cape
icy orbit
Does anyone know of a lightweight extruder that has a latch like clockwork 2 ?
T...
Neither one of those require any hands to load filament. If the tip of filament is cut at angle or sharp like a tip of a pencil, all you have to do is push in filament until tip gets in the gears. Then you do an extruder command. Maybe you need to push the filament a bit in beginning to get it going.
icy orbit
thorny cape
Neither one of those require any hands to load filament. If the tip of filament ...
Gotta try that, hope it's not requiring too much force to get a good first grip of the gears and that ot works with Bowden tube installed.
thorny cape
icy orbit
Gotta try that, hope it's not requiring too much force to get a good first grip ...
I have been doing it like this for a long time, since someone else told me the same thing.
Key is to have a sharp enough tip that gets between the gears so that when you push filament during loading, it gets pulled easily.
 versed wraith
@umbral scroll I am able to fully tension it, and it does not slip there
 umbral scroll
it's probably the latch part that catches on the screw being worn down too much or the arm expanding a bit, you'll have it bouce when you have it tightened and push down on it
versed wraith
Possibly, but I've been using this extruder for less than 10 hours printing time
umbral scroll
I know this is diff and it’s unlatched
But see if you can push that down/ bounce it
And see the thumb screw also move inwards when you push it down (while latched)
versed wraith
umbral scroll
But see if you can push that down/ bounce it
And see the thumb screw also move...
I can do this fine
umbral scroll
Like you can bounce it?
versed wraith
Uhh
umbral scroll
(With it latched not like my vid unlatched)
One sec let me latch it maybe that’ll be a bit easier
versed wraith
No, when it's latched it doesn't move at all
I have an inkling of what the problem is
From playing with it just now
umbral scroll
 versed wraith
umbral scroll
Isn’t there a heatset there
I should check
But not sure if it can be adjustable with a heatset
umbral scroll
Oh wait you might have it reversed
versed wraith
 umbral scroll
There should be a scre head there and it screws into the motor
versed wraith
umbral scroll
Oh wait you might have it reversed
i reversed it, i had it the correct way originally
umbral scroll
- chain thing
versed wraith
i must have lost an m3 washer, or never put it in
which would explain why the motor kept slipping out of alignment when placed under stress
umbral scroll
Well I didn’t expect that
versed wraith
which would cause inconsistent extrusion
and it to stop working after a while, which is exactly what i saw
umbral scroll
versed wraith
which would cause inconsistent extrusion
Yeah that might not be optimal
Also if that’s the fysetc gear check alignment with filament path
And see if you had washer come in the pack
Iirc they usually have a small washer in front and in back
versed wraith
umbral scroll
Also if that’s the fysetc gear check alignment with filament path
its the formbot, and everything is good, i have a whole bunch of spare washers
umbral scroll
versed wraith
its the formbot, and everything is good, i have a whole bunch of spare washers
Did the extruder have anything in the gear bag?
If not then don’t worry about it
versed wraith
probably, but i've mixed up everything now so i wouldn't know tbh
umbral scroll
It’d be a really thin shim
Like 0.1 or 0.2mm
If nothing sticks out then probably not + doesn’t matter too much anyways
deft flame
I'm struggling with choosing extruders between Sherpa mini (it derivatives) , orbiter 2.5, and wwg2. Largely because I can't really figure out what the pros and cons of each are. I get that they're all great but what is the reason one might choose one or the other?
 mellow cradle
at least a few reasons, I'm sure they are not exhaustive.
orbiter 2.5 = commercial extruder, no printing/assembly required, just pop it on and you're done.
wwg2 = you want galileo2 but in a bolt on extruder on the top type format
sherpa mini = lightweight/skeletonized, uses standard bmg gear drives and minimal printing required.
deft flame
Does anyone know for orbiter 2 smart sensor, what the nuts and washers included are for? I couldn't find any docs for assembly and am going by a single YouTube video that didn't mention them
 high spoke
Any thoughts on WW2 vs Sherpa Mini? Mainly for print quality I guess. I don't print flexible's, just PLA. No crazy speeds, building a Dragonburner soon and installing Dragon Ace, so maybe 30ish mm3/sec?
 shadow plinth
Why is there always a 1/2mm gap at the top of Stealthburner and clockwork 2?
 raven pewter
https://github.com/SartorialGrunt0/Awesome-Extruders
Ive been working on this list on and off for a few months. Let me know if you have any recommendations or extruders I missed.

GitHub
A collection of links to 3D printer extruders. Contribute to SartorialGrunt0/Awesome-Extruders development by creating an account on GitHub.
 tepid totem
Maybe this is a dumb question but I have a 12 tooth Nema 14 motor and I’m wondering if it would be fine to use it with a clockwork 2? The gear pitch seems the same so my thought was that I would just need to update the gear ratio/rotation distance
 raw compass
raven pewter
https://github.com/SartorialGrunt0/Awesome-Extruders
Ive been working on this l...
look mom, I made to the list 😄 😄
raven pewter
tepid totem
Maybe this is a dumb question but I have a 12 tooth Nema 14 motor and I’m wonder...
I’ve had this same question and haven’t tried it. I suspect the spacing between teeth might be a concern with gear meshing but I’m not sure.
Been debating just picking up a DXC extruder to use it with.
 subtle moon
Hey guys, I have a LGX steel drive train set I would like to put to use. Are there any opensource extruders that use this gear set with a filament sensor?
raven pewter
subtle moon
Hey guys, I have a LGX steel drive train set I would like to put to use. Are the...
How different are they from HGX lite gears?
subtle moon
honestly I am not 100% sure on this. I heard the HGX lite gears are clones of the LGX lite but I am not sure if this means they are they same gear sizes.
raven pewter
subtle moon
honestly I am not 100% sure on this. I heard the HGX lite gears are clones of th...
GitHub
Voron mods. Contribute to chirpy2605/voron development by creating an account on GitHub.
subtle moon
thanks!
 full pebble
Would I be able to use the internals from a BMG copy to make to the Clockwork extruder?
ruby pumice
full pebble
Would I be able to use the internals from a BMG copy to make to the Clockwork ex...
Clockwork or CW2 for SB?
Yes if you have all the parts the yeah, see the SB assembly manual to see which parts are used.
Also, #afterburner_and_stealthburner_questions
full pebble
CW2
ruby pumice
full pebble
CW2
Yeah, most parts lists just say "BMG kit" but doesn't break down the parts inside. So yeah look in the SB assembly manual to see what is used. It's something like this
https://kb-3d.com/store/bondtech/484-bondtech-bmg-extruder-internals-kit-build-your-own-1645151327973.html
I think the things in that picture are the minimum required
 broken fossil
I am trying to find the right discord channel. I am putting together my 2.4 and I am looking to put a rapidbuner toolhead on. I am using a WWG2 Extruder, and a Rapido 2 UHF. Looking at Chirpy's GITHUB, it is all over the place. can anyone point me the right direction?
ruby pumice
broken fossil
I am trying to find the right discord channel. I am putting together my 2.4 and...
#1182811180566331432
 proud stirrup
Anyone seen a comparison of these two CNC sherpa mini extruders? I haven't found anything


 rustic ingot
proud stirrup
Anyone seen a comparison of these two CNC sherpa mini extruders? I haven't found...
Same bmg style of extruder. Expect the same performance
 indigo swift
I have an older style stealthburner and I am considering reprinting the whole assembly due to potential fatigue and inserts showing signs of coming loose. Is abs still the right filament for longevity of the parts?
 native rapids
indigo swift
I have an older style stealthburner and I am considering reprinting the whole as...
yes, or ASA
indigo swift
Question: my stealthburner isn't grabbing filament anymore, the motor spins, I took it apart and couldn't find anything blocking it, is there some trick or thing to check that will make it obvious whats up? The idler arm moved freely
I can freely pass filament through to the hot end and it extrudes, even when closed up. It does seem like the top latch isnt snug however
ruby pumice
Check to see if that arm is cracked, that's the most common
BTW #afterburner_and_stealthburner_questions
indigo swift
Arm wasn't cracked, I think there was powder in the arm socket and it was preventing the arm from fully depressing against the filament
The grub screw was also a little loose and I feel great sadness I have no thread locker and I'll be tightening it again next year
But I'm resembling and I'll see how it performs now. I also found a ton of bolts loose and things misaligned, depression took a few years out of my printing but we're back baby!
 arctic flint
I'm working on a V0.2 made mostly from leftovers from my 2.4 (which got way out of hand). I have a spare standard BMG gear kit for a Stealthburner/Mini Stealthburner + the usual stepper. Are there any alt extruders I can use it with without needing to source anything exotic beyond the usual spares one accumulates? I think I can do the Sherpa Mini 2?
ruby pumice
Sharkfin is excellent
🦈
arctic flint
The aesthetic has me sold - it'll make the cat cowl on the Dragonburner I'm putting it on look like it has a mohawk
 carmine narwhal
Hello. I am sure this is my fault for not utilizing the PIF program, but I am not sure what I need to move forward.
 native rapids
carmine narwhal
Hello. I am sure this is my fault for not utilizing the PIF program, but I am no...
what issue are you perceiving? parts not fitting?
carmine narwhal
@native rapids cant get latch to close. Looks to me like it has interference in the picture and never going to close. I have had to get some of my printed parts replaced and have lost confindence that I even have correct printed parts for stealthburner. Not sure I have all the resources I am supposed to have for assembly, but I was moving forward until I started experiencing problems with my printed parts
native rapids
do the parts have any sort of elephants foot that you could trim off?
carmine narwhal
@native rapids i think the black plastic inside my blue circle is keeping the latch from closing. Seems like a lot to remove to me. Maybe one of my parts is wrong?
 native rapids
if all the parts were printed from one file source then different versioning is unlikely
your latch and shuttle look like the current versions
carmine narwhal
Thank You. I will remove enough material for it to work
proud stirrup
 ruby pumice
Just FYI for the last two posters....
#1182811180566331432
#afterburner_and_stealthburner_questions
 wintry dew
carmine narwhal
Thank You. I will remove enough material for it to work
I would suggest reprinting replacement parts as soon as you can as well. The latch is the newer stronger version and I would not recommend removing material from it and I would take it from the other side.
ruby pumice
Definitely don't remove material, that i the part most prone to breaking
 pallid grail
So I have my 2.4 (LDO kit), running the steathburner clockwork2 combo with a Revo hotend and TAP installed. It just doesn't seem to have any power to push filament, despite having a run current of 0.85, which I understand to already be high.
I also want more temperature at the nozzle, so I'm naturally looking at the revo high temp hotside. Should I be looking at a different extruder for more power, or maybe an entirely different setup altogether?
ruby pumice
pallid grail
So I have my 2.4 (LDO kit), running the steathburner clockwork2 combo with a Rev...
How fast are you trying to print? I'm not sure Revo is ever fast enough to outrun CW2
pallid grail
Even pushing 20 mm3/s of PlA with a high flow 0.4 is too much and it starts skipping. Shows I have plenty of heating capacity left, rarely above 80%.
Is it possible I have an issue with my CW2 somewhere then?
Swapping drivers never changed anything, did that a while ago.
ruby pumice
pallid grail
Is it possible I have an issue with my CW2 somewhere then?
Yes, it should have no problem going that fast. Hop into the right channel and check the pins for the videos to inspect the details of CW2 assembly. #afterburner_and_stealthburner_questions
Maybe it is the famous anti-squish
pallid grail
ruby pumice
Maybe it is the famous anti-squish
I jumped over there for troubleshooting, thanks!
carmine narwhal
@wintry dew @ruby pumice @native rapids my latch snaps shut now. Thanks
 rancid forum
which off the shelf extruder is best for flexibles like tpu 80A 70A
ruby pumice
rancid forum
which off the shelf extruder is best for flexibles like tpu 80A 70A
Is there a budget?
rancid forum
lets say no
ruby pumice
rancid forum
lets say no
Seems that nobody knows. Just not enoguh people watching this thread and the number ot people who take TPU seriously is probably low. Maybe consider Orbiter2, but also the Bondtech large gear extruders, like LGX Lite Pro which has multiple tension adjustments
I'm building a machine where TPU will be one of its jobs, using a Orbiter
WIth WWBMG, can you use standard BMG set like from CW2? @twilit solar
 river basin
ruby pumice
WIth WWBMG, can you use standard BMG set like from CW2? <@1266077934343426109>
OG Ww-BMG says BMG or RIGDA Gear Set in the BOM
wintry dew
@ember thicket I'm wondering if you looked at adding filament sensors to the ProtoXtruder 2.0?
Also, this seems to have quite a bit of play.

 rancid forum
ruby pumice
Seems that nobody knows. Just not enoguh people watching this thread and the num...
i have ordered a orbiter 2.5 with my voron kit i am going to put it on my custom toolhead hopefully
 ember thicket
wintry dew
<@763813061819367454> I'm wondering if you looked at adding filament sensors to ...
Yes.
- Extruder entry sensor: The extruder is too compact to directly cut out a built-in sensor. I'm still thinking about how to make one.
- Toolhead sensor: I've made some tests on a spacer under the extruder with a built-in sensor. Seems to work fine. Just need to spare some time to clean up and upload them.
Thanks.
wintry dew
I'm wondering if a small PCB with a detector switch can make both low profile: https://www.digikey.com/en/products/detail/panasonic-electronic-components/ESE-13V01D/822259

DigiKey Electronics
Order today, ships today. ESE-13V01D – Switch SPST-NO Surface Mount, Right Angle from Panasonic Electronic Components. Pricing and Availability on millions of electronic components from Digi-Key Electronics.
Or other similar switch.
Like this one can full stroke but then you need to deal with wear:
 ember thicket
wintry dew
Also, this seems to have quite a bit of play.
It's intended to have some slightly larger clearance to fit different prints. It should be fine to have that gear floating a bit there.
ember thicket
wintry dew
I'm wondering if a small PCB with a detector switch can make both low profile: h...
I'm more interested in using only common hardware. Also I have no experience making custom PCBs.
But I'd be super glad to see if anyone with better skills can take the CAD and make a sensor for it.🙂
wintry dew
I can handle the PCB stuff if we can find a nice one and a swich with enough force.
ember thicket
wintry dew
I can handle the PCB stuff if we can find a nice one and a swich with enough for...
That would be great! But sorry I have no further experience other than common mouse switches and button switches.😅
 wanton sandal
would anyone know the weight differences of, wwBMG wwG2 vs Sherpa mini CNC?
raw compass
wanton sandal
would anyone know the weight differences of, wwBMG wwG2 vs Sherpa mini CNC?
up to 20 grams
the weight is neglibile. G2 is the porker out of all these, CNC Sherpa is the best out of these because of metal frame but uses same gearset fit for RIDGA WWBMG extruder and I have made IDGA version for it which is essentially same shaft but idler teeth and filament teeth locations are swapped on the shaft
should you want to go for MMU, many recommend getting RIDGA parts and A4T extruder with filament sensor cutouts
for TPU etc, CNC Sherpa is against best out of these due to it's properly machined and depends less on your printer's accuracy and material tuning profiles. out of printed extruders they all should function just fine. my IDGA WW extruder mod pushed 95A TPU close to 30mm3/s with Peopoly Lancer Long without any issues through a 0.5mm nozzle.
there are more to extruders than just weight
wanton sandal
raw compass
the weight is neglibile. G2 is the porker out of all these, CNC Sherpa is the be...
Cnc sherpa is different from cnc sherpa mini?
raw compass
wanton sandal
Cnc sherpa is different from cnc sherpa mini?
its the same, im just lazy. Sherpa Mini and Sherpa Micro are different extruders. CNC versions are 99 times out of 100 always better
wanton sandal
raw compass
its the same, im just lazy. Sherpa Mini and Sherpa Micro are different extruders...
Thank you for the insight
 alpine haven
I upgraded from Afterburner to Stealthburner.
I replaced the stepper to LDO nema14.
I have issues with under extrusion for the infill. I think it is due to misalignment of the gear as I didn't adjust it and noticed that it was a bit loose.
I see over AliExpress Orbiter upgrade kit from 2 to 2.5. I believe the Galileo 2 is native to Voron.
Any insight what gear would be preferable to buy for an upgrade?
native rapids
alpine haven
I upgraded from Afterburner to Stealthburner.
I replaced the stepper to LDO nem...
Galileo 2 is a very nice upgrade to a stealthburner toolhead
ruby pumice
And I rally against trying to buy yourself out of problems 🙂
wintry dew
alpine haven
I upgraded from Afterburner to Stealthburner.
I replaced the stepper to LDO nem...
Orbiter =/= Galileo
They are different extruders and the one in StealthBurner is Clockwork 2.
ruby pumice
Yeah, G2 is in no way "native" to Voron
alpine haven
Is there a kit without the motor that is recommended?
Is there another popular replacement other than the G2?
I am running with umbilical
ruby pumice
OG BMG gearing (CW2 spec), IDGA BMG gearing (CW2), and G2E are the primary choices if staying on SB
#afterburner_and_stealthburner_questions btw
If you want to reuse the motor, IDGA is probably your best choice. G2E will not accept the 10T motor, it's has different gearing on the same motor
Recommend you just buy a real Bondtech set as it's pretty important for your results and not that expensive
raw compass
I'm at a point where I could use some extra torque. due to possible chamber temperatures of 70+C and me not having a HT stepper for extruder, can I replace the drive gear on the stepper? I figured the shaft is 2.5mm and there seem to be options for it both in brass and steel/iron. current gear is 10T, so going down to 8T or 7T would make sense if I dont want to add heat created by amperage. currently its set to 0.7A at 24V, stepper is stalling at 75mm3/s with ABS+ at 290C. what do, cheapest possible route 😄
 molten lily
raw compass
I'm at a point where I could use some extra torque. due to possible chamber temp...
75mm³?
What extruder are you running?
At that point 48v is probably something you could start looking into
 copper light
Hey-hey, people! Marry Xmax. I have a favor to ask, if possible. I'm as lazy as one gets. I bought voron 2.4 as my 2nd printer about 3 years ago. Aaand I have not done anything with it. It just works. (okay I installed cliky probe, cuz the metal sensor one never worked for me). So I saw the "Tool changer" mod for voron and kinda want it. So the question is... what toolhead + extruder combo should I get? not stealthburner. I tried researching it, but there are soooo many options and I'm getting overwhelmed by them. Please advise
native rapids
tool changers are not really for lazy people
but a better channel is #multimaterial_and_u
the combination rests upon which toolchanger method/system you choose, so
copper light
Yea, that's the problem, I hate choosing 😄
native rapids
stealthchanger, madmax, etc etc
copper light
I can dedicate time and effor for the assembly, but not reasearch of what is best. 😄 "MADMAX"! Thanks! I've been looking for the name
native rapids
it's still a niche of a niche, so some research is going to be required
copper light
I liked the design. Will go with it. Again, many thanks and merry christmass or your equvalent of holiday this time of year 😄
native rapids
 molten lily
copper light
I liked the design. Will go with it. Again, many thanks and merry christmass or ...
Madmax is awesome.
raw compass
molten lily
75mm³?
yes. I'm currently using my own mod for WristWatch extruder with MK8 drive gear and smooth idler. it started as an IDGA mod for WristWatch but 3 weeks ago I found MK8 drive gears from Ali and decided to order them and give it a try. so far I'm super happy with how it performs with TPU and harder plastics. had to increase the internal diameters a bit to fit the MK8 gear, rest is unchanged as its mounted on the same shaft with the 50T gear that BMG sets use. total cost for the gearset and bearings are like 7€. "rotation_distance: 4.05" with 10T stepper compared to 4.45 with RIDGA/IDGA, so there was some extra torque to be gained.
yesterday I had alonger ABS print going and after that I quickly re-energized the extruder stepper and took the measurements after some time. stepper peaked 86C in about 60C chamber, it's at 24V 0.7A. I have thought about 48V but CAN toolboards dont support it as it seems. other option would be to get 8T stepper or swap the stepper gear out by myself for 8T or 7T but can't find them anywhere for 2.5mm shaft, all offerings in the internet are for either 2mm or 2.3mm so redrilling would be needed should I order some.
 burnt fjord
Is there any difference in performance between sherpa and Wristwatch BMG?
They’re both BMG gear’ no?
 velvet solar
Just got a Beacon rev H and about to switch over from Dragon burner to A4T. I'm currently using CNC tap and wondering if it is worth having both Tap and Beacon? I have the space available on my toolhead board. I think I saw that tap is a little more accurate for z offset.
thorny cape
velvet solar
Just got a Beacon rev H and about to switch over from Dragon burner to A4T. I'm ...
No need for Tap and Beacon since Beacon has "contact" probing - same thing as Tap. Just use Beacon, it is perfect.
velvet solar
thorny cape
No need for Tap and Beacon since Beacon has "contact" probing - same thing as Ta...
That is what I have been leaning to. Tap has been working perfect for me just a little slow. I should get some more rigidity out of just doing beacon.
ruby pumice
I like Tap myself and have no plans to uninstall it. Up to you. If you've never done Beacon, I can suggest that as a learning experience since it's so popular now; I just installed my first one. Why are we talking in the Extruder channel? 😉
 cold epoch
what is e steps and gear ratio on clockwork 2
native rapids
cold epoch
what is e steps and gear ratio on clockwork 2
gear ratio is 50:10, stock rotation distance is 22.6789511 (will need calibration)
cold epoch
how do i change e steps in klipper if its posible
native rapids
we don't use e-steps in klipper, the term is rotation distance
you would use a calibration tool like https://tools.takuya.wtf/esteps.html
cold epoch
yes but how do i change the code for klipper to do the change
native rapids
open your printer.cfg in mainsail or fluidd's web interface. find the appropriate line of code. make your change. save and restart the firmware.
cold epoch
ok
native rapids
i presume this is not for a voron
cold epoch
well for stealtburner cw2
 neon dragon
The red graphs are hotend temperature and power during temperature calibration print.
The hotend is rapido plus 2.
Before this print i've performed the pid calibration and saved the config.
I suppose the instability is not normal.
What can be the problem?
 neon dragon
After more search i've found that manually reducing pid_kp might help
The difference is immense (this is a different print, but the picture is clear)
For now i will continue monitoring, but i assume the problem is incorrect pid calibration
 wintry dew
Or is this the print cooling fan turning on?
neon dragon
The print cooling fan was on the whole time.
The instability was present even without printing in process, when setting hotend to a temperature.
 lofty abyss
guys can you share your own orbiter v2.5 rotation distance i want to compare it with my calibration
 void sequoia
Hi all, is there a specific good go-to for HGX 2.0 gears? I’ve had a couple of these running with great results for a while now. I bought two more set of gears and they’re not concentric. Thanks.
 wintry dew
void sequoia
Hi all, is there a specific good go-to for HGX 2.0 gears? I’ve had a couple of ...
Ohh, what body is that?
void sequoia
wintry dew
Ohh, what body is that?
My own design. Wanted an LGX Lite but didn’t like the price. 😂
wintry dew
I like the design. Is it shared anywhere yet?
void sequoia
wintry dew
I like the design. Is it shared anywhere yet?
Not yet. It’s pretty much done, but I want to make sure my gear distances are based off a gold-standard gear set and not just any random set from AliExpress or Amazon. I’ve gotten wildly undersized gear sets before so I want to make sure I have a specific brand that I can recommend.
wintry dew
@raw shadow and I had been recently talking about the gearset as well. In the protoextruder 2.0 I made, I'm not sure how much the second gear will do for driving and I'm considering making it with a smooth idler.
 raw shadow
void sequoia
Hi all, is there a specific good go-to for HGX 2.0 gears? I’ve had a couple of ...
that looks great!
i like that extruder
void sequoia
wintry dew
<@239626226115936256> and I had been recently talking about the gearset as well....
The first two sets I got from Haldis on Ali are currently the best and don’t seem to have any issue. Just want to be sure.
 low crater
Looks really cool
void sequoia
Thanks!
 meager isle
printing an extruder in a gf/cf filament... good idea, bad idea, doesn't-matter-all-that-much idea? My only worry would be the abrasiveness of it might mess with feeding filament, but that might be overthinking it
molten lily
meager isle
printing an extruder in a gf/cf filament... good idea, bad idea, doesn't-matter-...
Doesn’t matter at all. Make sure that it is somewhat temperature resistant though or you will have to lower your extruder motor current
meager isle
cool cool. shouldn't be any worse than what i run normally--going to use gf-asa
 elfin granite
hey does anybody know where i can find the STL for a WWBMG with dual filament sensor? or recomendations to use with the cross bow. thanks
river basin
elfin granite
hey does anybody know where i can find the STL for a WWBMG with dual filament se...
It is in the A4T github, this version is using the Sherpa mini spacing.
 ashen ether
Hey guys, I'm looking into an A4T with a dragon ace volcano. I was looking either at a WW-BMG or WWG2 for the extruder. What do you guys think? (Orbiter looks cool too)
@elfin granite cool profile pic
river basin
ashen ether
Hey guys, I'm looking into an A4T with a dragon ace volcano. I was looking eithe...
I use WW-BMG and i have been very happy with the quality, i almost went for a g2 but i had a stepper motor already and just needed a RIDGA kit so it was a lot cheaper that way “make sure to get the Bondtech if you go with that route”
Here is an example of my ASA prints

 ashen ether
That looks awesome
I ended up ordering a g2 kit, sorry😅 I really appreciate you sharing this though cause I currently only have a neptune 4pro and an unassembled v0.2. Right now the wwg2 is going on the n4pro. I'm still going to re-evaluate what I do to the v0.2 if and when I get there cause I just went with a basic kit and making it go a little faster sounds like a lot of fun
river basin
ashen ether
I ended up ordering a g2 kit, sorry😅 I really appreciate you sharing this thoug...
No worries, im sure the g2 will be great. I have a V0.2 too, the prints above was done at 8k acceleration and 220mms
ashen ether
That's awesome. My plan is to make the v0.2 my dedicated ABS/ASA machine with an internal filtration unit of some sorts and then put up some type of airtight enclosing around it to make it safe long term to live with. It's good to see other people having some good success
river basin
ashen ether
That's awesome. My plan is to make the v0.2 my dedicated ABS/ASA machine with an...
I have a mini carbon filter and a sealed printer and got no issues with smell, but i do understand that others might be more worried about the particles from ABS
ashen ether
That's good to know man
untold ivy
Can someone help me? I have a step file id like to put a filament sensor in it if possible.
I suck as cad..
Id like a 5.5mm ball with a d2f
 low parrot
Hello, maybe it's not the right channel here, so tell me if I'm wrong.
I do have stupid extrusion issues with my Voron 2.4 350 since around a half of a year, making my motivation to work on it nearly zero.
Now let me come to the issue:
Nearly all prints I do will have no filament coming out of the nozzle after a while.
If I push the filament ever so slightly in again it will continue and work for a while.
First I thought its maybe a issue on the filament inlet / path. I switched the tubes and shortened the path, made sure there are no bends or hard corners.
It did not do anything. I switched the extruder gears, I calibrated the CW2 many times.
Nothing worked.
After a while I thought maybe its a heat creep from my dragon HF hotend, but even with a way more powerful fan its still the same issue.
The hotend is also not really clogged, I can pause the print and then extrude filament and it will just work fine, even tho it just stopped in the print.
I thought maybe its a issue with the fact, that my CW2 parts are printed in MJF (Nylon) but a friend has the same and he does not have the issue.
The gear's do have quite good contact with the filament, and do not directly slip when I pull on it, but it is also not impossible that it gets out if I pull to much.
I'm actually out of ideas and don't know what to do anymore.
I hope some people in here can help me figure it out and solve it hopefully.
Thank you already guys.
untold ivy
I think your grip isnt good.. you may need to reprint the parts... if you put filament in and hold the gears. The filament shouldn't slip out
It could be the latch...
Or the extruder parts themselves
low parrot
untold ivy
Or the extruder parts themselves
They are printed in MJF (nylon) and a friend has the same without a issue. I did also order the same extruder parts then him and the issue gets actually even worse with them.
I'm getting confused by the extruder gear washer that are included and no not know where they need to go. https://de.aliexpress.com/item/1005005663309821.html
Also the big gear has a lot of play in there. Latch gear is fine. The MR85 on the CW2 main body has also a lot of play in all directions and can fall out easier (checked CAD motor plate has 8.1mm and CW2 main body has 8.2mm)
untold ivy
I would check to make sure the filament isnt slipping
raven pewter
void sequoia
Hi all, is there a specific good go-to for HGX 2.0 gears? I’ve had a couple of ...
Did you finish the design? If so do you have a github link?
void sequoia
raven pewter
Did you finish the design? If so do you have a github link?
Not yet, the last two sets of gears I bought weren’t concentric so I’m still on the hunt for a reliable source to fine tune the design around.
raven pewter
void sequoia
Not yet, the last two sets of gears I bought weren’t concentric so I’m still on ...
Truth be told, they are all probably from the same Chinese factory haha.
void sequoia
raven pewter
Truth be told, they are all probably from the same Chinese factory haha.
Haha yeah probably. Makes it a little challenging.
raven pewter
void sequoia
Haha yeah probably. Makes it a little challenging.
How much does the concentricity matter on these? I’ve built a couple HGX extruders without checking the concentricity, they seem fine 🤷♂️.
I suspect think the larger gears are less sensitive to it.
ruby pumice
 keen falcon
If anyone knows more about WWG2 I'd appreciate any assistance.
#1160715888048218193
 neat sinew
What's the consensus these days with cnc extruders? I am 100% wanting to go cnc but I am kinda torn between the sherpa mini or the hextrudort.
Wonder if anyone might have any thoughts on which one would be better.
ruby pumice
Considered Bondtech?
raven pewter
neat sinew
What's the consensus these days with cnc extruders? I am 100% wanting to go cnc...
There is a TriangleLabs CNC Sherpa mini that’s cheap and well built
molten lily
neat sinew
What's the consensus these days with cnc extruders? I am 100% wanting to go cnc...
some of those have trouble with conducting too much heat into the filament and causing jams on certain filaments at high motor current. The two all metal extruders that seem to have fixed the problem are lgx pro metal and sherpa v3
sometimes cnc isn't always better for some applications
neat sinew
molten lily
sometimes cnc isn't always better for some applications
I print 99.5% ABS/ASA. I am always dealing with Printed Extruders loosening up every 5 hours or so.
molten lily
neat sinew
I print 99.5% ABS/ASA. I am always dealing with Printed Extruders loosening up ...
Oh you should be fine. I would get a sherpa v3 if you are set on cnc. Or you could wait for the lgx lite pro metal
that will be soon
neat sinew
molten lily
Oh you should be fine. I would get a sherpa v3 if you are set on cnc. Or you cou...
I will keep an eye out, I really do love the WWG2 but I am past having to tighten them up nearly everyday.
Thank's for the insight.
molten lily
neat sinew
I will keep an eye out, I really do love the WWG2 but I am past having to tighte...
What did you print the wwg2 out of? You might want to print it out of something semi crystalline
(not a nylon though)
neat sinew
molten lily
What did you print the wwg2 out of? You might want to print it out of something ...
I've done a few in ABS from Various Vendors.
I have PET-CF and PPA and PPS CF but have not really dived into the annealing needed for them.
molten lily
neat sinew
I've done a few in ABS from Various Vendors.
I have PET-CF and PPA and PPS CF bu...
You should try it out with that pet-cf and anneal it.
neat sinew
Currently the 2 WWG2 I have deployed are using Fusion's newest ABS that has to be printed at 295c minimum.
neat sinew
molten lily
You should try it out with that pet-cf and anneal it.
I have a WWG2 printed out in the PET-CF but just have not annealed it yet.
molten lily
neat sinew
I have a WWG2 printed out in the PET-CF but just have not annealed it yet.
I would just try that before you buy a new extruder because wwg2 is already a good extruder. You wouldn't really be doing much of an upgrade
neat sinew
I may give it a shot and see how it works out.
molten lily
you can try that pps as well. I like pps it is fun to drop on surfaces
neat sinew
molten lily
you can try that pps as well. I like pps it is fun to drop on surfaces
I like the PPS but it seems to be very sensitive to part cooling fan. If I run enough fan for overhangs it really messes with the layer adhesion.
The PET-CF is a joy to print as it really hardly needs any fan at all even for some pretty steep overhangs.
molten lily
neat sinew
I like the PPS but it seems to be very sensitive to part cooling fan. If I run ...
yeah you just need support interfaces for a lot of engineering polymers
 quaint field
I cant really find anywhere official to ask for help with the orbiter, so ill try here to see if anyone has experienced this. I have an original orbiter 2.5, and every time i change filament, it gets stuck like this. I have to either cut it into a very sharp point, or often i need to open the extruder and manually guide it in
 ruby pumice
quaint field
I cant really find anywhere official to ask for help with the orbiter, so ill tr...
Official Orbiter talk is on Facebook (big groan)
Every time, or when you are at the inner part of the spool which has a real tight diameter?
You can also try cutting a much sharper angle
quaint field
ruby pumice
Official Orbiter talk is on Facebook (big groan)
Ugh, I think I'd rather buy a different extruder than go on Facebook again
It's every time. I can usually avoid it by cutting at a much sharper angle, but even then it sometimes takes a couple of attempts. I think it happens no matter where on the spool I am, but it's probably worse at the center
 torn epoch
hi, does anybody here use a4t toolhead with "Modified WW-BMG with Bondtech RIDGA v2"?
i have an issue that when printing petg with higher speed it tends to slip, i mean i am using the smooth tension arm and that might be the issue but its also seen as an upgrade over the regular arm
so i am not sure what to do, no matter how much i increase the tension the petg stays unsquished and it slips, like it gets grinded at some point and it stops completly
i might switch to the regular arm but then i wont have the benefits of the smooth arm
ruby pumice
We know what wwbmg is, you’ll have to be more specific about what the modified version is
How fast are you trying to print? PETG doesn’t print that fast afaik
torn epoch
ruby pumice
We know what wwbmg is, you’ll have to be more specific about what the modified v...
500mm/s peak speed
torn epoch
ruby pumice
We know what wwbmg is, you’ll have to be more specific about what the modified v...
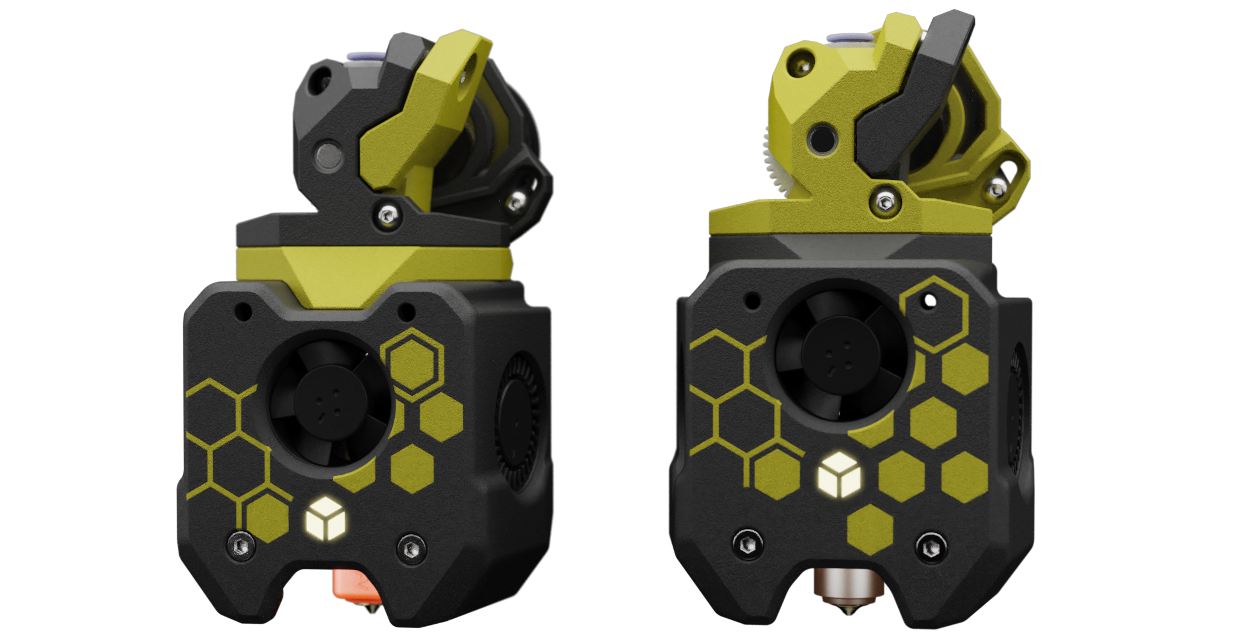
GitHub
[A]nother [4]010 [T]oolhead. A toolhead for Voron front rail printers built around 4010 blower fans, efficient ducts, and easy assembly. - Armchair-Heavy-Industries/A4T
this version
ruby pumice
torn epoch
500mm/s peak speed
Ever printed PETG that fast?
torn epoch
it was working in another print
maybe it wasnt maxxing the speed as much?
like accel might have limited it
there is this one print
that at the same point each time
ruby pumice
A lot of things can limit the speed, you have to verify in the speed view to check
I'm just wondering if you can lay down PETG at that speed
torn epoch
the only problem is the extruder
what if i get a different one?
a better one?
ww-bmg is recommended for a4t for some reason
ruby pumice
I have no idea, I've never printed anywhere near 500mm/s
torn epoch
ok
ruby pumice
Why aren't you asking over on the Armchair discord?
torn epoch
i didnt knew about it
thx for letting me knoe
actually the invite seem to not work?
 violet zodiacBOT
 minus1ms has been warned
Reason: Posted an invite
torn epoch
ok
thorny cape
quaint field
I cant really find anywhere official to ask for help with the orbiter, so ill tr...
Strange, I have been using Orbiters 2.0 and now 2.5 for maybe 3 years, since 2.0 came out. I don't have issues with loading filament at all. I do cut filament in a point but in general I have no loading issues.
Couple of things to check:
Use reasonsble tension; I turn tensioner 8 or 9 half turns.
Check instructions on Orbiter 2.0 page on how to screw in that metal filament guide after the gears. It must be just not touching the gears.
Make sure drive gear teeth are aligned with filament guide; you might need to use one or few shims to push back the gear.
 tidal hollow
Hi everyone,
I’m running a Voron Trident: Stealthburner + CPAP, LGX Lite, Dragon V2 hotend (80 W).
I want to increase flowrate, and I’m unsure if I should just upgrade the hotend or also the extruder and go for a new toolhead like XOL.
I’m considering Orbiter or Galileo with Dragon ACE with Extender—are these still current/recommended options for high-flow printing with 0.6–1 mm nozzles?
Any advice for high flow would be much appreciated!
molten lily
tidal hollow
Hi everyone,
I’m running a Voron Trident: Stealthburner + CPAP, LGX Lite, Drago...
If you want to increase flow rate you should mostly be looking at a new hotend.
If you print with large nozzles you should be looking at hotends with huge meltzones: CHC XL (questionable) goliath, tricorn, mosq magnum+, chube air, chube conduct ect
tidal hollow
molten lily
If you want to increase flow rate you should mostly be looking at a new hotend.
I’m aware of that, but I’m not sure if my LGX Lite will handle it. If I need to change the extruder too, I’d probably redo the whole toolhead (maybe XOL) and switch to an eddy probe instead of Clicky.
That said, I’d prefer to keep the LGX Lite if possible.
My budget is around 100 € in the EU (ideally Spain). I’m currently looking at:
Dragon ACE MZE (~80 €)
Rapido Plus 2 HF (~99 €)
molten lily
tidal hollow
I’m aware of that, but I’m not sure if my LGX Lite will handle it. If I need to ...
I have had really bad experiences with rapidos of all kinds. I used to run them a lot. Dragon ace volcano (DAV) is the way to go for a reliable budget mid flow hotend.
raven pewter
tidal hollow
I’m aware of that, but I’m not sure if my LGX Lite will handle it. If I need to ...
LGX Lite should be fine. You will almost always outrun your hotend first. If not, try increasing extruder motor current a bit until it does.
 tawdry path
So far i have used HGX lite etruder variants. I have no experience with BMG type extruders. For toolchanger i wamt to keep it budget so i want to do DB with bambu hotend and WW-BMG extruder as a cheaper version of WW extrduer. So anyone running WW-BMG to coment on experience, performance, issues?
 round crane
Need help. I want to use dual filament sensor in my extruder for mmu. But i runout endstop pin on my sht36 v3 toolboard (for x endstop, klicky probe, and filament sensor). I can realocate the x endstop but that mean more cable through the gantry and i hate more cable  . is there any pin i can use for my second filament sensor?
wintry dew
round crane
Need help. I want to use dual filament sensor in my extruder for mmu. But i runo...
If you are using at PT1000 then you can use the thermistor port as another endstop port.
round crane
wintry dew
If you are using at PT1000 then you can use the thermistor port as another endst...
Oh really? Which one is it?
wintry dew
I don’t understand your question.
round crane
wintry dew
I don’t understand your question.
Which one did i use for the endstop in my sht 36
wintry dew
round crane
Which one did i use for the endstop in my sht 36
I don’t know how you wired your board.
round crane
 wintry dew
This is my board with an add on PCB I made to make wiring the sensors and fan easier.

Most GPIO can be inputs other than:
- GPIO24 output only
- GPIO26 (RGB) output only
round crane
wintry dew
This is my board with an add on PCB I made to make wiring the sensors and fan ea...
Oh wow thats insane. Did you had the design file?
wintry dew
round crane
Oh wow thats insane. Did you had the design file?
I have not released it yet.
arctic flint
I’m officially over fighting against the design of the Stealthburner, and now I have an MMU I want a more robust cutter than Filametrix (no shade on the project I just can’t get it working reliably myself - skill issue).
Given I’d like to keep using my CNC tap, am I correct in thinking A4T with a crossbow is the way to go? I’ve ordered myself an Orbiter 2.5+filament sensor and have an EBB36 gen2 which I’m pretty happy with.
raven pewter
arctic flint
I’m officially _over_ fighting against the design of the Stealthburner, and now ...
There isn’t a ton of filament cutter options out there for Voron toolheads.
Here is some options if you filter by filament cutter: https://toolheadbuilder.gallinetwork.com/toolhead-builder/
Toolhead Builder
Find compatible toolheads by selecting your extruder, hotend, and probe.
molten lily
arctic flint
I’m officially _over_ fighting against the design of the Stealthburner, and now ...
If you go for an mmu setup you will want something that is really close cut. The best option is probably something like RX toolhead. A4t also cuts it really close to the hotend
 hybrid fog
So, if I go a 8:60 gear ratio for the extruder I’m getting more force but will I run out of push at higher flows?
rancid forum
hybrid fog
So, if I go a 8:60 gear ratio for the extruder I’m getting more force but will I...
bigger gear ratio = stepper motor needs to spin faster, but it delivers more torque
wanton sandal
Would fyset cnc sherpa mini be a good extruder or do i have to change some parts from it like the peek gear? Not really familiar with all the different type of gears and the recommended ones
molten lily
wanton sandal
Would fyset cnc sherpa mini be a good extruder or do i have to change some parts...
No, the v3 sherpas are pretty good
wanton sandal
molten lily
No, the v3 sherpas are pretty good
Awesome 👌
 slender glacier
Anyone know what a reasonable temperature on a stealthburner extruder motor should be? Measured on the outside "shell" of the motor.
An LDO-36STH20-1004AHG(XH)
There are no fans so i would think it runs hot?
I have run_current set to 0.5 and measure about 70 degrees C.
Having issues with print stopping, du to no filament extrude (sensor), i manually have to push 0,5-1 CM of the filament down then its good to go.
Then perhaps 5 min later i have to repeat.
Some times it can run 1 hour.
On a 4 hour print it has stopped 10 timed, currently watching it and its been ok the last 30 min.
Could it be that my motor is running to hot and causing a soft stall of some sort?
ruby pumice
slender glacier
Anyone know what a reasonable temperature on a stealthburner extruder motor shou...
Don't know, I never measure mine. Normal run for that motor is 0.60-0.65A
Might be worthwhile to disassemble and see if you have an assembly problem
slender glacier
ruby pumice
Don't know, I never measure mine. Normal run for that motor is 0.60-0.65A
Ty, I thought I read about that. Dunno how I manage to put 0.5 there.
I’ll try 0.6 and print again, but I noticed a possible issue.
The PTFE tube, are there any specifications for ID?
Couldn’t find anything specific, but, I saw some pictures online that showed a little tighter ID than what I had installed.
native rapids
slender glacier
Ty, I thought I read about that. Dunno how I manage to put 0.5 there.
I’ll try ...
the reverse bowden tubing should be 3mm ID. the piece between extruder and hotend should be 2mm ID.
slender glacier
native rapids
the reverse bowden tubing should be 3mm ID. the piece between extruder and hoten...
Perhaps that all along could be the culprit… I used 3mm ID…
Did feel for every “stop” that I had to manually push the filament into the hotend, 5-10mm or something. Kinda felt some resistance.
Possibly hitting the outer rim of the hotend? 🤷🏻♂️
 normal tiger
chasing an issue of skipping in the extruder. Once and a while I can hear it give a click click click while extruding, sometimes in only one specific part of a print. Had a look at my gears and they look okay but the drive gear on my clockwork 2 is able to slide fairly readily on the gear shaft. I don't recall if this is normal or not from the original build but I'm guessing that it is not.
If i pull on the filament while it's extruding i can feel a "dead spot" where it stops and then starts again. It prints rather nicely still though beside these issues so i'm rather confused. I feel like this would cause more of a problem.
wintry dew
normal tiger
chasing an issue of skipping in the extruder. Once and a while I can hear it giv...
Yeah, that set screw should be tight. The other failure point would be if the gear driving the shaft has cracked and is loose on the shaft as well.
normal tiger
I ordered the "Bondtech BMG IDGA Retro-fit Set" which appears to include the entire shaft assembly
ruby pumice
yeah, that's basically what IGDA is
normal tiger
i was able to repair the set screw but after reassembling the motor is skipping
i'm not sure if i overtightened something or it's misaligned
normal tiger
this is the same noise that I was mentioning before but it appears worse now.
wanton sandal
So i tried using sherpa mini cncn by fysetc, and in regular filaments its ok but in abrasives it keeps on jamming?
I lowered tension and also tightened tension, i tried to baby step the tension to the point that it will just grab the filament and when pushing through hot end, i tightened it little by little but still no luck
 tiny oriole
Whats the "best" extruder for abrasive filaments? the CW2 cant grip my CF nylon good enough
molten lily
wanton sandal
I lowered tension and also tightened tension, i tried to baby step the tension t...
Are you either printing extremely slow with a high motor current or outrunning your hotend by pushing too much filament?
molten lily
tiny oriole
Whats the "best" extruder for abrasive filaments? the CW2 cant grip my CF nylon ...
You may want to try and repackage the gears in your clockwork into a sherpa mini. The tensioner is a bit more robust
wanton sandal
molten lily
Are you either printing extremely slow with a high motor current or outrunning y...
Either the one i have had bad tolerance or it is by design anyways i widen the exit points and it actually works now
molten lily
wanton sandal
Either the one i have had bad tolerance or it is by design anyways i widen the e...
Oh ok good 👍
wanton sandal
molten lily
Oh ok good 👍
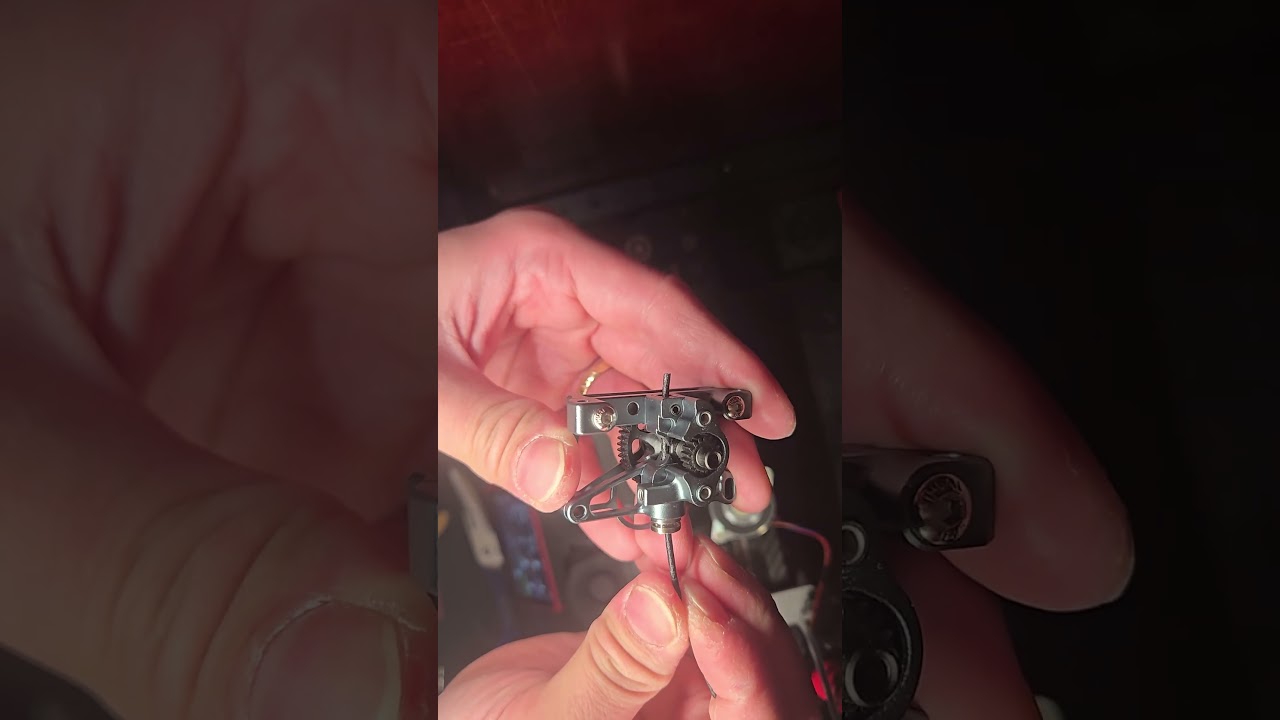
Not sure if this issue for this one is a known or my luck is just terrible
molten lily
wanton sandal
Not sure if this issue for this one is a known or my luck is just terrible
Looks like you have bad luck
I would contact fysetc
wanton sandal
I reached out to them too but havent heard back
tiny oriole
molten lily
You may want to try and repackage the gears in your clockwork into a sherpa mini...
Interesting
Oh but it doesn’t work with stealth burner?
 wintry trout
i think ive settled on the wristwatch g2 as a good lightweight planetary gear single drive extruder, but am i missing a newer option? i dont really know what my options are outside of that
i know of the two sherpas which seem nice but i wanted to use single drive
ruby pumice
wintry trout
i think ive settled on the wristwatch g2 as a good lightweight planetary gear si...
That's a good choice, my memory is fading, Orbiter is in the same family but dual-drive
https://discord.com/channels/460117602945990666/1160715888048218193
wintry trout
gotcha, yeah, i was just looking around for a low backlash single drive extruder
i like my sovol ace's planetary extruder but for my own printer and for upgrading my old ender i wanted something lighter and single drive based on what i saw from vez, 247printing, the orbiter blog and elsewhere
and just, for something different too
anyways, i guess ill get one of those, seems like the g2sa internals or kit are around 45$ which isnt too bad i guess
ruby pumice
yeah, I run both the G2 and O2, haven't decided which I really favor. But G2 can be built more compact (than O2)
wintry trout
iirc the planet gears are metal and not plastic right? or am i misremembering
oh, nevermind, i think i see everything i need to know on the github :D
ruby pumice
yes, both those extruders are pretty well documented if you read
 red mesa
I'm having issue when printing : "extruder" not hot enough. My printer used to work fine until recently. I did : PID_CALIBRATE HEATER=extruder TARGET=210
PID parameters: pid_Kp=29.179 pid_Ki=2.138 pid_Kd=99.576
The SAVE_CONFIG command will update the printer config file
with these parameters and restart the printer.
But I still get that same error when launching a print ; "extruder" not hot enough . Anyone knows what I can do ?
native rapids
red mesa
I'm having issue when printing : "extruder" not hot enough. My printer used to w...
i would suggest posting a summary of your issues in #1169407804386316288 with a klippy log, this is not related to your extruder but will be related to your print start macro
red mesa

 acoustic lantern
What's everyone's go to extruder these days?
 knotty gazelle
acoustic lantern
What's everyone's go to extruder these days?
The question is usually very specific "it depends".
Easy disassembly for cleanup? Pushing force? Looking cool? Weight? Size? Is it for toolchanger? Being cool and rather unusual?
Probably won't go wrong with Orbiter 2.5, Galileo 2 in one of repacks, Wristwatch BMG or one of Sherpas.
Papilio if you want something unusual.
acoustic lantern
I've ran Orbiter, Sherpa and recently the BIQU Nebula. I'm just looking got consistent extrusion quality
knotty gazelle
There's more into that than just extruder alone. I had Clockwork 1 on Switchwire and it made really nice prints. Trianglelab BMG gears.
But it also had Dragon SF and printed considerably slower 😄
People like G2, but it has bearing instead of second driven gear, thus pushing (or pulling) force may not be as high as Orbiter.
acoustic lantern
I keep getting artifacts in my prints that resemble z banding and I'm positive it's from the extruder. Just looking at some other options.
knotty gazelle
What printer? It could be real Z banding, bed not PID tuned, varying part cooling fan, motor pulley being tilted...
have you tried (R)IDGA to address potential drive gear eccentricity?
raw compass
acoustic lantern
What's everyone's go to extruder these days?
WW MK8
 gentle kite
I've been unhappy with the Stealthburner on my Trident recently, mostly with the steps of disassembly when it comes to jamming and the lack of feedback when tensioning. I haven't been paying too much attention to developments over the last few years so I'm not sure what's around. Dragonburner was the "it" thing last time I checked.
If I'm looking for something simple but modern with TAP and suitable for UHF, what extruders should I be looking at? Ideally I'd like to reuse my EBB SB2209 if I can.
native rapids
gentle kite
I've been unhappy with the Stealthburner on my Trident recently, mostly with the...
sb2209 is only really easily compatible with stealthburner, without using some weird adaptors
and are you asking more about the whole toolhead, or just the extruder
gentle kite
I guess that makes sense looking at the SB...
Toolhead would have been the better term. I'm set on the hotend I have (Dragon UHF) but the rest I'm open to changing, although preferably I'd wanna keep what I can from the SB out of frugality
ruby pumice
I'm with you on tensioning, it has not driven me crazy lately but is a problem. But honestly none of the other extruders I know of have anything, they are all zero feedback tension screws. It makes me lust after a Bontech extruders until I see the prices
And yeah, RIP SB22xx. Unfortunately EBB36 is used on basically everything else
gentle kite
I'm trying to knock out something in TPU right now so the tension issue really shows there
ruby pumice
yeah, one thing I "miss" about the Prusa was that you could be crude and count the number of threads showing at least. On SB you can probably do something similar with the antisquish screw
 near orchid
Just a general question. I currently have a sherpa mini (3d printed frame), but have some issues with seam on prints. Can upgrading to a different extruder help improve seam?
ruby pumice
near orchid
Just a general question. I currently have a sherpa mini (3d printed frame), but ...
Probably not, which hotend do you have with it?
near orchid
ruby pumice
Probably not, which hotend do you have with it?
TZ-V6-2.0 with HS 0.4mm
Generally print with ASA
 steady pumice
Hey all, I have a possibly dumb question but always good to get a sanity check
I'm putting together the Miró extruder and it's all gone very smoothly, but when I run some filament through it, unless the tension is almost completely released I basically cannot move filament through it, the guidler arms look way more splayed out than they probably should be, almost like the smooth idlers are protruding too much but I've triple checked and the parts are printed correctly and they're pressed in as far as they'll go, is this normal or have I done something wrong ?
 native rapids
@honest swallow or @gray phoenix may be able to help.
steady pumice
Some pics of how the bearing sits in the arm, if that's of any help


Pic with the bottom smooth idler + top geared, the smooth one just seems so splayed out

 honest swallow
steady pumice
Hey all, I have a possibly dumb question but always good to get a sanity check
...
Yeah those arms are definitely way too far; it seems it is the smooth bearing at the bottom that is causing it to be that far
What's the size of the bearing you are using? Can you take a measurement of the diameter using some calipers?
It seems larger than spec'ed.
steady pumice
Annoyingly my calipers ran out of battery the other day but i do have a sinking feeling i maybe ordered the wrong ones, they're MR85ZZ bearings from trianglelab
honest swallow
the shaft looks larger than 5mm, looking at the pic it seems it is not sitting deep enough in the part
steady pumice
The shaft is a 5mm OD 8mm length steel cylindrical pin, which i believe is what was specified in the BOM
I'm truly baffled
honest swallow
I would suggest measuring it when you get new batteries

This is the separation on mine
steady pumice
Yeah that's more what i was expecting
honest swallow
5mm shaft 8mm bearing
steady pumice
I think it must be the printed part somehow as the pin fits the bearing perfectly, and i tried several other MR85ZZ's i had on hand with the same result
I tried printing it in a few different orientations just to see if that'd make any difference at all but nope
honest swallow

Make sure there is nothing in between then of you are sure
Take a pic of the Miro with the idlers out
Curious if something is in the way


 gray phoenix
it looks like the 5mm shaft is not completely snapped in please measure the 1.4mm ....
 steady pumice
hmm yep that's what i was thinking too
steady pumice
Okay I figured it out thanks to your diagram, they were indeed sitting too far out, why exactly I'm not sure, could be due to the 0.5mm nozzle I use in my printer or it could be yet more Arachne nonsense, I used my soldering iron to sink a pin deeper into the slot and now it works perfectly, will do some testing to see why the holes are not printing deep enough before I print the final ones
Thanks very much for your time @honest swallow and @gray phoenix I really do appreciate it
steady pumice
Oh also you should release that weird mod you did for the mellow cannon, I really wanna build that
wintry dew
void sequoia
Not yet. It’s pretty much done, but I want to make sure my gear distances are ba...
How goes your testing?
void sequoia
wintry dew
How goes your testing?
Well, they technically work pretty well but I keep buying different gears and they keep not being concentric. I’m considering switching back to the original Bondtech style gears because I can at least buy quality ones.
 turbid wigeon
Do I need a clip here to “secure” the push-in collet?
ruby pumice
Yes of course, but it's not to stiffen it I think, it's to prevent the release of the tube
turbid wigeon
Is there a printed one? I can’t find anything on printables
ruby pumice
turbid wigeon
Is there a printed one? I can’t find anything on printables
Oh, I've never looked. Most of us have them lying around everywhere. It didn't come with any?
turbid wigeon
No, no collect clips with LGX extruder
ruby pumice
I could be completely wrong, I don't own any of this fancy Bondtech stuff
turbid wigeon
Can’t even find a collet clip for ecas04
ruby pumice
Do the product picture show it....that is what I would reference
native rapids
https://www.printables.com/model/135121-collet-clip-for-ptfe-tube something like this
Printables.com
A better-fitting collet clip to reduce retraction issues | Download free 3D printable STL models
ruby pumice
It's not in their product pictures; I'll just switch to "I don't know". I think you should do whatever seems logical based on your experience holding it
native rapids
Could always ask in #bondtech what they recommend
ruby pumice
I'm jealous of your extruder, I would love to have a Lite Pro on one of my printers
 deft galleon
The clip is generally only used for remote extruders connecting via bowden, not direct drive configured extruders
river basin
honest swallow
You might wanna print an extra, there is a hair line crack by the bottom screw
raw compass
Miro caught my attention but remixing is not allowed, so off the list it goes. there's just one integrated support for the whole set of parts whilst there could be more to ease printing or modify the tension arms to be printed without supports.
Sherpa Crew Redux seems to be older design, but with lower center of gravity even with its taller design due to having the stepper sit about 5mm lower and printing it is that much more bulletproof.
just my 2 cents.
 neat belfry
So I am starting to wear out my teeth on my BMG gears. The gears are wearing out as they no longer grip the filament. The teeth are being worn down.
The extruder I am using are sherpa mini's. I cannot use the ridga gears because they will not fit into the triangle lab sherpa mini's I am using. What BMG gear set do you all recommend.
native rapids
neat belfry
So I am starting to wear out my teeth on my BMG gears. The gears are wearing out...
Have you ever used bondtech brand, or have they all been generics?
neat belfry
native rapids
Have you ever used bondtech brand, or have they all been generics?
I have used bondtech, and generics. However, I don't really have data on which last longer.
But, I am coming to a point to where I am wearing out multiple bmg gears, and I do not know which is which
native rapids
Hmm. You print many more miles of filament than I do, but for me years of abrasives use has never left a dent in bondtech gears. I’m not aware of anything better BMG wise, my other suggestions would be exploring larger gears/g2 etc.
ruby pumice
not the drive teeth I guess
neat belfry
@ruby pumice the teeth which contact the filament
ruby pumice
Dremmel some new teeth?
ruby pumice
neat belfry
So I am starting to wear out my teeth on my BMG gears. The gears are wearing out...
Maybe try the Runice coated ones? They have a matte color so you'll be able to know later which set you're looking at
It just came to me, I think they called it DLC coated. Or is that just stuck in my head from gaming? I'm not sure....
neat belfry
ruby pumice
It just came to me, I think they called it DLC coated. Or is that just stuck in...
Rnc coated?
ruby pumice
neat belfry
Rnc coated?
RCK coated?
neat belfry
ruby pumice
RCK coated?
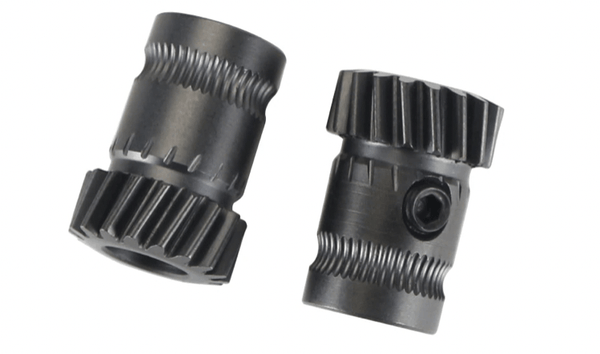
West3D 3D Printing Supplies
This helical gear set is designed to maximize torque and wear resistance for double gear extruders like the V1/V2 and Sherpa. Nano-coated for increased service life, it ensures optimal durability and performance.
ruby pumice
neat belfry
https://west3d.com/products/hardened-rnc-helical-gear-for-double-gear-extruders-...
Well....we all know that you should never order helical ones
neat belfry
ruby pumice
Well....we all know that you should never order helical ones
why is that?
ruby pumice
someone post "the picture" please, I'm looking on AliE for the Runice ones
Runice BMG-style clone internals kit with RNC-coated drive gears for abrasive filament, Voron-era extruder builds, and BMG rebuilds.
https://www.fabreeko.com/products/bmg-kits
Out of stock at Fab
wintry dew
wintry dew
neat belfry
why is that?
See the pin from RCF.
neat belfry
wintry dew
See the pin from RCF.
I do not see the pin
wintry dew
neat belfry
I do not see the pin
The forward above is the pin.
mellow cradle
the short answer is because CW2 was not designed to work with helical gears.
blissful barn
wintry dew
So what happened?
blissful barn
ruby pumice
Well....we all know that you should never order helical ones
I do not see why helical gears are a problem, I also do not see why they should "maximize torque", have any influence on "wear resistance".
native rapids
the issues are explained in the forwarded post and conversation that follows. the forces generated are not ideal for our applications
blissful barn
They just reduce noise at high speeds and you can tweak the center to center distance, using them. Plus they look cool.
blissful barn
native rapids
the issues are explained in the forwarded post and conversation that follows. th...
I wonder how high the forces actually are, but given the very questionable claims about improvements it is probably academic.
I would claim the main function is to "look fancy".
native rapids
which is of course very highly important for a part deep inside your extruder system. /s
blissful barn
native rapids
which is of course very highly important for a part deep inside your extruder sy...
Black opaque panels is the next big thing. One thing the helical gears are good at. You can make very small pinions with a few teeth only, which could give you some extra ratio. But that counts only when used for motor shafts.
 mellow cradle
Your DIY printer is your DIY printer. Do what you want.
just we don't recommend helical extruder gears for our extruders. 🙂
 stable stirrup
hey guys i have a stealth burner extruder that doesnt grip very well. when tighten or losen the idler knob it doesnt really change it. just grips weakly and eventually strips


Like should the teeth not be bigger to grip it?
 native rapids
Everything in those pictures needs a severe cleaning before we would be able to comment further. Those gears have seen some things….
stable stirrup
i re did it and cleaned it feels great now
raw compass
stable stirrup
hey guys i have a stealth burner extruder that doesnt grip very well. when tight...
time for a toolhead swap and WW IDGA build
stable stirrup
lol
 wind ocean
Hi voron wizards, I'm planning my doom build and need some pointers
Will there be any benefits/tradeoffs with upgrading to Bondtech lite pro (normal and/or slm viersions)? Haven't looked into the big gear hype yet so I'm hoping someone can give me a place to start.
Ideally I want single "all-rounder" printer (fast+quality) and lots of abrasives (75% of printing) .
Thank you
current parameters:
using allmetal wwbmg RIGDA v2 gears w/ 6T LDO.
No issues currently, prints fantastic for my speeds/accell 300-400mm/s @20k dragon uhf mze 0.4mm diambondback with plans to push speeds. No heatsoak issues for now.
Waiting for chube air to ship for takeofff.

 hybrid fog
@timber zealot HGX gears can be used for these extruders
https://www.printables.com/model/822947-protoxtruder-20
https://www.printables.com/model/367706-hummingbird-extruder
https://www.printables.com/model/404246-large-gear-clockwork2
some food for thought

Printables.com
The sequel of ProtoXtruder. New gears, thinner, and lighter. | Download free 3D printable STL models
Printables.com
A compact extruder with high torque and good filament grip. | Download free 3D printable STL models
Printables.com
Voron Clockwork2 with large extrusion gears. | Download free 3D printable STL models
 rigid vale
hybrid fog
<@658192062948048896> HGX gears can be used for these extruders
https://www.p...
I quite like the design of the ProtoXtruder 2.0
I even modified it a bit to allow for easier cleaning/unclogging without the need for a single Allen key

 tawdry path
So im running WWBMG with DB on my 2.4. The potential issue im fasing is short overlap between stepper gear and extruder pom gear.

The thickness of extruder back plate or where the bearing sits has not been modified....
IMO it is either the bmg gear is outof spec or stepper gear offset is different...
Either way i cant push bmg gear further in to the back plate...
Will inspect when i get home...
native rapids
tawdry path
The thickness of extruder back plate or where the bearing sits has not been modi...
would be useful to know which parts you printed and motor model/source when you have a chance.
rigid vale
your printed parts do not fit all that well
 native rapids
The texture on the motor plate does concern me a bit
tawdry path
native rapids
The texture on the motor plate does concern me a bit
it is abs gf
tawdry path
native rapids
would be useful to know which parts you printed and motor model/source when you ...
A couple more picture. IMO the printed parts came our very acurate and nice..


Stepper is no name chinese frome ali express. From black surface around the gear to the top of the gear is 5.5mm

For Voron 2.4 NEMA14 36mm Motor Round Pancake 6BYG1204-A-6QHT for Orbiter Sherpa 3D Printer Voron Mini Extruder
https://a.aliexpress.com/_EwUFUbU
native rapids
Hmm the gear on that looks fairly normal. Trying to think where the misalignment is coming from.
tawdry path
I have another set printed since im doing toolchanger
Will assemble thar one as well
rigid vale
tawdry path
you say the printed parts came out very acurate but they clearly don't fit well
the dovetails between the main body and the motor are being pushed apart so the parts don't line up
tawdry path
BMG Extruder kit Dual Drive Gear Hardened Steel Upgrade Feed Gear Extruder Kit For BMG For Prusa DIY Bowden Direct Extruder
https://a.aliexpress.com/_EHIpj7Y
tawdry path
rigid vale
you say the printed parts came out very acurate but they clearly don't fit well
...
Maybe slight missaligment

I think this is due to heat my heat insert
rigid vale
it's the 3 dovetails
maybe the parts are overextruded
I'm sure you can scrape the inside with a blade or a small file and make them fit better without reprinting
but they clearly don't fit well right now and they're twisting the assembly
tawdry path
Slightly better?
 rigid vale
a bit better gear engagement but still not ideal
if the parts came out overextruded and don't fit you might need to scrape off some more
tawdry path
rigid vale
a bit better gear engagement but still not ideal
if the parts came out overextru...
But where ?
rigid vale
you can see at the top that the edges still don't line up
the dovetails aren't fit well
rigid vale
tawdry path
But where ?
the whole interface between the motor plate and the main body
it was very visible thanks to the dovetails, but if the parts are overextruded, it's the whole interface
tawdry path
 rigid vale
that's why your motor is sitting further back than it should
tawdry path
rigid vale
that's why your motor is sitting further back than it should
But the bearing is almost through the back plate
If i measure the thickess of the back plate together with bearing in it is 3.15mm
rigid vale
well I can't inspect your parts for you and I don't have the CAD model in front of me, but the dovetails show that they were not printed acurately, so the fit is not good
maybe it's not just the GF that made them look a a bit bumpy
perhaps they got scaled to compensate for shrinkage twice? once by the designer and a second time by your slicer?
tawdry path
Hmm
rigid vale
tawdry path
in any case, you can see in almost every picture how the assembly is bent and twisted due to the poor fit
tawdry path
rigid vale
well I can't inspect your parts for you and I don't have the CAD model in front ...
Also is this much slack ok
rigid vale
because the gears are barely meshing at all
the motor plate is twisted out of position
tawdry path
rigid vale
because the gears are barely meshing at all
the motor plate is twisted out of po...
Another one assrmblrd. It is a bit better i think
 rigid vale
it does look better
have you dried your filament well?
the fibers make it hold moisture better and that could be the cause of overextruded parts
hmmm
though even if the parts were perfect it seems that your motor is still gonna be sitting a bit too far back to mesh fully...
tawdry path
rigid vale
have you dried your filament well?
the fibers make it hold moisture better and t...
Yes
i think it is cheap gears as well
this one is much better atleast it has no slack on the gears
rigid vale
yeah, more acurately printed parts will help with that
tawdry path
I will mount this one and do a test run..
wintry dew
tawdry path
Also is this much slack ok
That would be too much in my opinion.
tawdry path
Ok new extruder, up the current in extruder from 0.6 to 0.8 amp. Turn on arc fitting and i kind of like the results a lot. This is from bottom 18mm3/s to the top at around 25mm3/s. Vase mode..
rigid vale
hehe I knew it wasn't the hotend reaching its limit
 tawdry path
rigid vale
wait why is it slowing down in the middle of a straight line?
Dont know yet.
Need to ask wise people at duet forum about that
rigid vale
well if the printer is slowing down like that maybe the flow numbers you expect are not what you're actually getting...
wintry dew
rigid vale
wait why is it slowing down in the middle of a straight line?
Seam position?
tawdry path
Probably, but im still satisfied fith results
rigid vale
it happens more than once per loop
and a vase mode flow test should have no seams
tawdry path
Especialy stacking
 tawdry path
Well, it is much better now that i turn on arcfitting
Where did i put yesterday tests..
hmm looking at g code i cant see any G2 and G3 commands so orca did not prosses arc fitting ?
rigid vale
🤷🏼♂️
should leave for the appropriate channels now that the extruder issues are gone, tho
tawdry path
yeah. Thank you for all the help. really appreciate. 🙂
 cosmic jewel
has anyone else had issues with the WWG2 ECAS and automated filament loading? the filament seems to keep getting stuck in the ECAS somehow
near orchid
Is there a good resource for common extruder comparison? I currently have a printed sherpa mini, but the bearing holder cracked so i was looking to upgrade
native rapids
near orchid
Is there a good resource for common extruder comparison? I currently have a prin...
near orchid
this website is nice, but it only provides technical specifications. I have a hard time understanding why one extruder might be better than another. i was looking at galileo 2 because of higher gear ratio for more precise control. Is there any reasons one should pick one extruder over another?
i guess i am interested in the different strengths of each extruder for given application
near orchid
tawdry path
almost looks like maybe really bad input shaper settings?
native rapids
near orchid
this website is nice, but it only provides technical specifications. I have a ha...
Mr @potent python is very good at explaining this sort of thing if they are available.
 potent python
Im here, hi
potent python
near orchid
speedy
Boss man called 😄
near orchid
mostly what each one is good at
or why i would pick one over the other and for what reason
for reference i have used the stock afterburner mini and sherpa mini on a V0 and didn't really notice much difference
potent python
If you're looking for a simple sherpa mini swap, wwbmg is a great choice. There is one in the a4t repo at armchair github that has a few nice advantages over sherpa mini while retaining sherpa mini mount spacing.
potent python
Notable differences are
The idler arm has more bulk, is less likely to bend
The bearing sits in a polyhole, which reduces stresses and prevents cracking
The heatset insert for idler tension is replaced with a square nut so it would have to pull through the whole plastic, rather than pull out.
near orchid
potent python
If you're looking for a simple sherpa mini swap, wwbmg is a great choice. There ...
after looking at this one, i think i also used this one for a little bit too
potent python
near orchid
i would say "end game" extruder
Its actually exactly what i use. and i highly recommend it useually, with a rigda gear from bondtech. But i can give you a rundown of my other personal faves too
near orchid
my main question is why someone would choose G2 over something like sherpa mini or WWBMG
potent python
Orbiter 2 or 2.5 is excellent off the shelf, and great value tbh. Very decent extruders.
Galileo 2 is probably the best widely available extruder for wall quality. It has a large, very well machined gear and produced very consistent flow.
8t bmg varients have a ton of torque, have a low center of gravity normally, and are decetly light and simple and normally affordable. Rigda brings them to a place where they are in the ballpark of the other 2 above. Its splitting hairs but g2 is better ime.
Lgx lite pro is also meant to be really good and i like it a lot on paper, but its like €120 so i dont own one.
near orchid
120 euro for an extruder is nuts
potent python
I dont tend to recommend anything with worm drive, as they tend to like 48v and frankly i suspect they lose a lot of potential power to friction losses. Spur gears are ~99% efficient. Worm gears can be as bad as 50%, maybe 70-80% if its well setup
near orchid
i do have concerns with the flow consistency, but don't really have any other way to test it other than vibes
its caused by AB motors or extruder and i figured that changing extruder first would be cheaper/easier
potent python
theres 2 things that can happen. You get small scale repeating patterns (20mm of ome layer), caused by tooth to tooth problems, cause your gear mesh is loose. Or you get large scale (miltiple layers) patters caused by the hobbed gear being off center of the axis of rotation.
Rigda specifically is made to be very closely aligned to the axis of rotation. Thats why it costs a bit more.
G2 really took this far too
potent python
well
near orchid
almost def caused by motors
potent python
Are they strictly vertical?
near orchid
yes
potent python
Then yeah thats motion not extrusion
near orchid
i think i will try going back to ww bmg because g2 would require new motor
if i decide to get ridga, would you recommend getting the whole set, not just the 50t+drive?
potent python
G2 kits come with the motor. They also need proper gears and the carrier and the planet housing and you shouldnt be printing any of that for good results
near orchid
potent python
G2 kits come with the motor. They also need proper gears and the carrier and the...
kits are $50
potent python
near orchid
if i decide to get ridga, would you recommend getting the whole set, not just th...
Just the 50t gear is fine tbh
near orchid
wwbmg is basically filament lol
potent python
near orchid
kits are $50
If it helps you feel more efficient with your hard earned money you can tell yourself its the better choice cause wwbmg has more torque and less weight. Tho honestly, thats not a huge deal in most setups.
But id be really surprised if you didnt like rigda. Just make sure the backlash with the motor is minimal.
Its the rigda oem v2 you need for wwbmg
near orchid
https://west3d.com/search?type=product&q=ridga
west3d only has the set
West3D 3D Printing Supplies
West3D specializes in sourcing and selling the best 3D printing products at affordable prices supporting makers across the world. Sold and shipped from the USA.
tawdry path
near orchid
almost looks like maybe really bad input shaper settings?
No imput shaper
near orchid
or the v1 by itself
tawdry path
It was just low jerk,..
potent python
Also, print a spare idler arm just in case. You never know, and its like 5p in filament
tawdry path
I got it dialed in now. Works nice..
near orchid
I assume the middle and right ones are v1?
 potent python
near orchid
https://west3d.com/search?type=product&q=ridga
west3d only has the set
Surely in the Us there is someone else...
potent python
near orchid
I assume the middle and right ones are v1?
They are IGDA, which has the hobbs far from the 50t and are backwards for most printed extruders.
near orchid
shoot ridga vs idga
rigid vale
@potent python sorry to butt in but I too am curious about extruder selection
is there any reason you'd recommend against using this one:
https://github.com/nhchiu/3DPrinter-Designs/tree/main/ProtoXtruder_2.0
I don't have enough experience with different extruders to say but I quite like the open design using those large gears
near orchid
no worries
potent python
near orchid
no worries
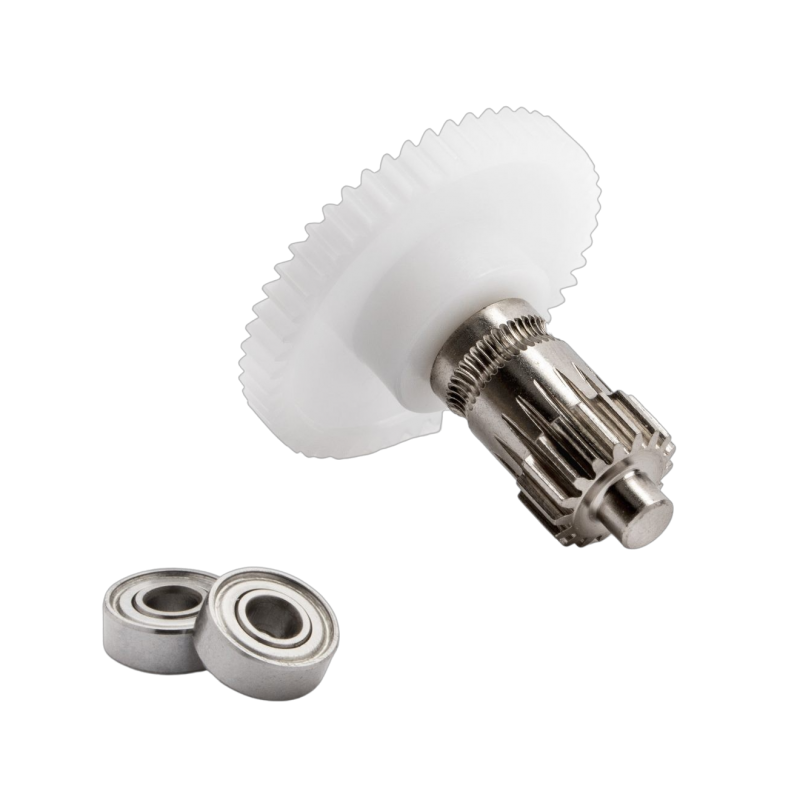
KB3D
Eliminate tolerance laden connection points with Bondtech's reverse integrated drive gear / shaft assembly. Combines the main BMG primary gear with the shaft for improved concentricity.
near orchid
my current drive gear is from formbot, so questionable quality
potent python
I would avoid the metal rigda unless you have direct, actual need for HT filament. Otherwise it just conducts motor heat into the filament, and wears out brass motor gears.
potent python
rigid vale
<@195286997240250368> sorry to butt in but I too am curious about extruder selec...
I dont have any particular problem with that extruder. Its maybe unecessarily complex/heavy, and no one i have heard has raved about its print quality. But conceptually it could be very good with decent quality gears. I dunno tbh. Its almost certainly fine no doubt. I think with rigda wwbmg available it would have to be better than fine to be something id suggest anyone ever run and all i know for sure is that its heavier.
If you have lgx lite and think its having gear mesh problems, there a really fun solution for that

Literally just shove the motor closer to the first gear, and it gets better they say
rigid vale
potent python
I dont have any particular problem with that extruder. Its maybe unecessarily co...
Okay thanks
I am not chasing the absolute best print quality as I really only do functional parts
I wanted an extruder that would have a better chance of printing super soft filaments like SEBS thanks to the larger gears
and also be easy to open to clean up in case it still grinds the filament
potent python
Oh, large gears are a mixed blessing
Tpu, sebs, pebs, they'll find any hole they can and pop out of it right
rigid vale
hehe they do
potent python
Now, especially with printed extruders, its really hard to get the filament path up to the gears
Its even harder with bigger gears to close that front and back gap
rigid vale
Yea I can see that, but spaghetting out of the extruder is not the most common issue I've had with the soft filaments
SEBS specially gave me a ton of issues with grinding between the gears as it is soft and rubbery like an eraser
I hope that lower pressure between the gears would help me print with that successfully in the future
I also modified the design a bit to make possible opening it up without tools, for when I eventually have to clear any such issues
 potent python
rigid vale
Yea I can see that, but spaghetting out of the extruder is not the most common i...
sounds reasonable.
rigid vale
I don't mind trading a bit of print quality if it means the print doesn't fail halfway due to grinding
that SEBS stuff is hell ngl I have had so many failures
potent python
If you do get issues, you could cut some ptfe tube to a sharp point, and slide that into the bottom of a modified housing.
Or buy some stainless steel tubing even, im sure 2mm ID is available on amazon or whatever
rigid vale
ah that's a good idea
bore a 4mm though hole and line the thing with a sharply cut PTFE piece
rigid vale
I'll seriously consider doing that when I build my next toolhead
that's quite a good idea, given how difficult it is to print a sharp filament path in there
potent python
rigid vale
hmm any reason to choose PTFE or SS over the other?
The path to the hotend in the toolhead is already made for a piece of PTFE so it could be a single one all the way from the gears
potent python
Ptfe will be lower friction and kinda hard to cut straight and not that strong.
SS feels lile itll be easier to get in a useful shape, slightly more friction, but we already use it in hotend so it cant be that bad right? orbiter uses SS
Would behoove us to find a way to key said tube into place as well. To stop the pointy bit from spinning into the gears
near orchid
potent python
Its actually exactly what i use. and i highly recommend it useually, with a rigd...
you're in the readme. biased source
potent python
near orchid
you're in the readme. biased source
Am i?
near orchid
GitHub
Contribute to bythorsthunder/Voron_Mods development by creating an account on GitHub.
potent python
Aww, nice.
potent python
near orchid
https://github.com/bythorsthunder/Voron_Mods/blob/main/Wristwatch_Extruder_BMG/R...
https://github.com/Armchair-Heavy-Industries/A4T/tree/main/STL/WW-BMG for A4T
I recommend this one
GitHub
[A]nother [4]010 [T]oolhead. A toolhead for Voron front rail printers built around 4010 blower fans, efficient ducts, and easy assembly. - Armchair-Heavy-Industries/A4T
Slightly changed, all for the better imo
near orchid
should i still be able to put this on dragon burner?
or should i replace my DB with A4T
potent python
This one uses sherpa mini spacing
So, uhh, yes?
Should fit absolutely fine. DB has lots of room
DB is really performant for its size and stuff. Changing toolhead is out of the scope of my cares right now 😄
Im gonna play some video games for a bit. Feel free to tag me with questions, but replies may be significantly delayed 
near orchid
potent python
https://github.com/Armchair-Heavy-Industries/A4T/tree/main/STL/WW-BMG%20for%20A4...
don't have square nut
also requires ecas 4mm which i do not have
maybe worth the purchase of those parts though
potent python
Ecas i say absolutely. I think square nuts are really good to have on hand too. Very affordable. Very easy to design for if you plan on doing any cad at all
near orchid
potent python
Ecas i say absolutely. I think square nuts are really good to have on hand too. ...
what is the advantage of ecas
i don't even understand what it is really
near orchid
@potent python, i do have a separate question that you may know the answer to. when i print the ww bmg, the bearings do not press fit. however, they are not super loose. are they supposed to press fit when printed?
pretty much when i turn the parts upside down, the bearings do not fall out, but they are certainly not snug either
potent python
near orchid
i don't even understand what it is really
Oh its just a ptfe tube holder really. Springy metal ring that grips inside a housing. It doesnt let go, and i think its generally better than push fit.
potent python
near orchid
pretty much when i turn the parts upside down, the bearings do not fall out, but...
So the one i linked is not a circular hole. Its designed to have less stresses. It should stay put on its own. I guess if its loose enough that itll fall out by tapping it on a table you might want a bit more flowrate on the print
near orchid
potent python
So the one i linked is not a circular hole. Its designed to have less stresses. ...
I just put the worlds smallest dab of super glue on the bearing to hold it in place
near orchid
potent python
Oh its just a ptfe tube holder really. Springy metal ring that grips inside a ho...
maybe i do have one
near orchid
just for sake of discussion, the sherpa mini was fine, but two of the parts failed
one cracked like this (which was repairable with super glue)

the other cracked like this

I have a feeling the first one was from overtightening the screws
but the second one is just from the fitment of the shaft
near orchid
i am building ww bmg
 zealous cargo
Yea I dont remember my other one being this hard to turn by hand, and the motor plate sat flush im pretty sure.
near orchid
not the exact one you sent
i think your 50T is on backward
can't really tell from the video you sent
zealous cargo
 zealous cargo
Yeah..
 knotty moon
Is this from a cheap BMG kit or are these bought separate gears
 zealous cargo
near orchid
i think this spacing should not exist
if i push the gear inward any more it rubs on the plastic housing
near orchid
can you try to assemble without that gear?
take it off the shaft entirely and just leave the idler
if it closes without it, that might indicate the spacing is not supposed to be there
zealous cargo
uh arent they typically glued on
zealous cargo
https://a.co/d/0ihL4Q9U got this guy based off a recommendation by @quartz cave
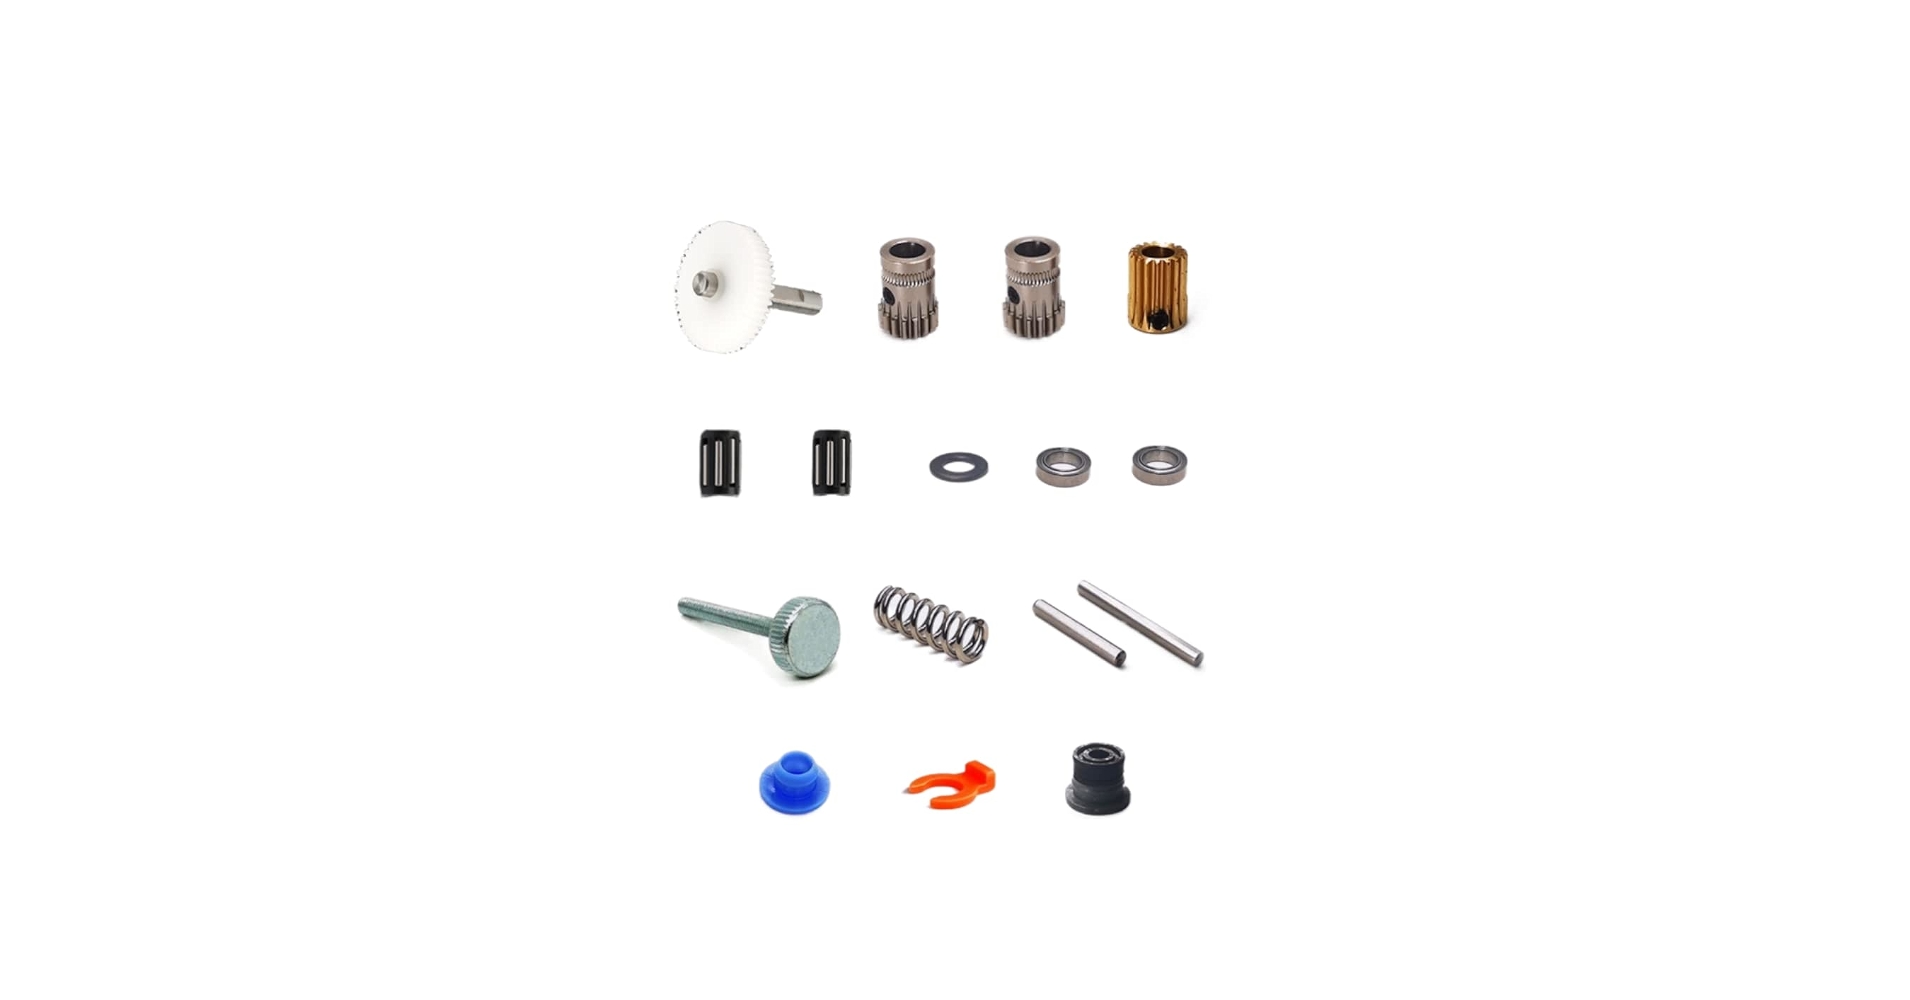
3D Printer BMG Accessories Reduction Mechanism AB extruder GEA kit for Voron V0.1/1.8/2.4
 zealous cargo
Oh I thought u said to take the white gear off, which doesnt have a set screw..
near orchid
miscommunication
keep the 50T on and remove the filament drive gear
i am not sure if the 50T is glued or if it is press fit
but i had to assemble mine with the formbot kit i bought, so i assume it is press fit
zealous cargo
the reason im using this specific IDGA version of the wwbmg is because i wanted to ruse the gears from my formbot kit lmao
zealous cargo
near orchid
i think you need to adjust the placement of the white gear then
zealous cargo
https://www.formbot3d.com/products/voron-24-r2-pro-corexy-3d-printer-kit-with-m8p-cb1-board-and-canbus-wiring-system?VariantsId=10457 got the 350 from here, this gearset im using rn is NOT the one from the formbot kit, the formbot gears went together fine

FORMBOT 3D Printer
Voron 2.4 R2 Pro+ CoreXY 3D Printer Kit with M8P+CB1 Board and Canbus Wiring System
near orchid
ok
zealous cargo
they werent adjustable from idga to ridga like the set from amazon
near orchid
maybe i didn't
i really don't know
i have only used the stock v0 extruder, ww bmg, and sherpa mini
i am unsure which if any are idga or ridga
zealous cargo
maybe my backplate warped from taking it off the bed too fast and thats why it doesnt sit flush with the gear in, idk lmao
near orchid
 near orchid
zealous cargo
maybe my backplate warped from taking it off the bed too fast and thats why it d...
possible
does is rock when you put in on the table?
also please verify if there is 3mm or less on the one end of the shaft
i would imagine you'd want the same spacing for that extruder, but i can't be sure because i am unfamiliar
zealous cargo
3.16 i think..
i feel like maybe the gear is slightly too wide or something to fit in the cavity for it
idk
near orchid
that would be weird
does the backplate rock back and forth on a flat table?
aka is it warped?
zealous cargo
Doesnt seem to
near orchid
how thick is the 50T gear?
zealous cargo
3.25
near orchid
the bondtech idga set says 3
but again
.25 doesn't seem like it would make a difference
are the bearings set properly?
zealous cargo
What do you mean by that..
near orchid
the bearings on either side of the drive shaft have little holes where they fit in to the plastic housing
are they set in the bottom of those holes?
I will send a ss, give me a sec
zealous cargo

 zealous cargo
yeah
 zealous cargo

https://github.com/minilogique/ww-extruder-for-idga/blob/main/STLs/WWBMG BEEFIER MOTOR PLATE.stl now he does have a "beefier" motor plate available..

GitHub
WristWatch extruder for IDGA gearset. Contribute to minilogique/ww-extruder-for-idga development by creating an account on GitHub.
not sure if that means more room for the gear or what
ahhh rip.. #1512544878716784690 message
i just noticed the designer's note in there
"friction. depending of the used mechanical parts and printer setup the main parts are printed with, putting too much tension on the bolt that holds the tension arm can bend the motor plate piece and flex, so it rubs heavily against the 50T gear and causes unneeded friction. also if you're using 2-piece BMG gear meaning not the billet version but the one with the shaft without a flatspot and BMG gear with grub screw, if the grub screw stands too tall, it can also run against the printed main body. because I personally have not experienced that, I have not accounted for that. if that is the case, do let me know."
well the grub screw isnt sticking too high but the main gear is rubbing..
near orchid
so forgive me, but why are you using this extruer instead of normal ww bmg?
zealous cargo
IDGA gear support.
near orchid
but isn't the kit you bought interchangable?
zealous cargo
Yeah but I wanted to make them all match.. I guess they dont HAVE to
i have a stealthchanger
near orchid
i get that
zealous cargo
would be weird to have tool 1 be a different extruder but yea i guess it doesnt matter
near orchid
ah i wish i knew you had a thread open for this
near orchid
zealous cargo
would be weird to have tool 1 be a different extruder but yea i guess it doesnt ...
ig, but there really isn't an issue wanting it all the same
zealous cargo
im confused
near orchid
i'm saying there is nothing wrong with wanting all the extruders the same
zealous cargo
ah ok
near orchid
i don't think i will be more help than minilogique
zealous cargo
tbh
maybe i should just use a "standard" extruder for this tool and if it works out, spend another 15 bucks and rebuild the original with this also..
zealous cargo
not doing myself any favors going a route that only 1 other person has gone
zealous cargo
https://github.com/PrintersForAnts/AntHead/tree/main/STLs/Extruders/BMG any idea why there are 2 different tensioner arms and why one is accent color the other isnt..?
GitHub
Toolhead for Micron and other PFA printers . Contribute to PrintersForAnts/AntHead development by creating an account on GitHub.
near orchid
couldn't tell ya
zealous cargo
crap that ones not sherpa spacing
Alright well i guess ill reprint the O2 anthead body with the regular WWBMG..that should work..
near orchid
i think a4t makes a sherpa spacing wwbmg?
near orchid
potent python
https://github.com/Armchair-Heavy-Industries/A4T/tree/main/STL/WW-BMG%20for%20A4...
this one @zealous cargo
zealous cargo
I just printed the new anthead body that has orbiter 2 spacing and kept the stock wwbmg
Thanks for that though
near orchid
np
zealous cargo
The print is already going 😅
near orchid
only reason i knew that existed is because weaslus spoonfed it to me
too bad i was out
near orchid
putting the ecas on is peak
 halcyon lintel
question which i feel is simple but also can't find a direct answer. but for a voron 2.4 that will start with a stealthburner and eventually be a stealthchanger. I kinda just stuck on was extruder to go for. the sherpa mini/micro seems like a good old classic thats well received. but orbiter 2.5 is newer and the orbiter series in general seems liked a solid choice.
so ya any help would be appreciated. because i don't need the best of the best, just reliable and works, and aint gonna break the bank.
native rapids
halcyon lintel
question which i feel is simple but also can't find a direct answer. but for a v...
There are only really two extruders that work well with stealthburner- the default clockwork2 and the alternative galileo2. The Sherpa and orbiter are for alternative toolheads.
halcyon lintel
native rapids
There are only really two extruders that work well with stealthburner- the defau...
given i am looking to eventually upgrade to a mini burner for the stealthchanger system. and a lot of cross compatible . though seems the Galileo2 uses a modifed standalone version for the mini burner. so 3 mentioned above all technically work in the final toolhead of the mini, but not all are 100% supported in the normal burner. because thats the case, what would you recommend. Since i'm not in a rush to build my voron then upgrade it.
zealous cargo
Welp...that looks suboptimal...
native rapids
halcyon lintel
given i am looking to eventually upgrade to a mini burner for the stealthchanger...
Well, both cw2 and g2 have parts that can be “repacked” into other extruders.
halcyon lintel
native rapids
Well, both cw2 and g2 have parts that can be “repacked” into other extruders.
thats a fair point, and if nothing else the ldo motor most likely can be pass on atleast saving a good 30 bucks
zealous cargo
Any idea why this extruder is all loosey goosey
I printed a different one with the same settings and it didn't do this
knotty gazelle
zealous cargo
they werent adjustable from idga to ridga like the set from amazon
Sidenote - the whole point of "Integrated Drive Gear Assembly" is to have shaft and drive gear milled from single piece, to avoid runout caused by possible eccentricity caused by putting drive gear on shaft and securing with set screw.
IDGA abd RIDGA are sold in configuration you choose, because the drive gear cannot be moved.
The set you say that "can be changed from IDGA to RIDGA" is a standard BMG set (or a clone).
You can't change IDGA to RIDGA, you need to buy a new single piece.
 quartz cave
zealous cargo
Any idea why this extruder is all loosey goosey
I’d run with it. I think at least one of mine is like that. The filament once loaded will hold it in place.
zealous cargo
knotty gazelle
Sidenote - the whole point of "**Integrated** Drive Gear Assembly" is to have sh...
I mean...I ran it in both configurations last night, one with the extruder path close to the big gear and one with it further away

Thought that was the difference?
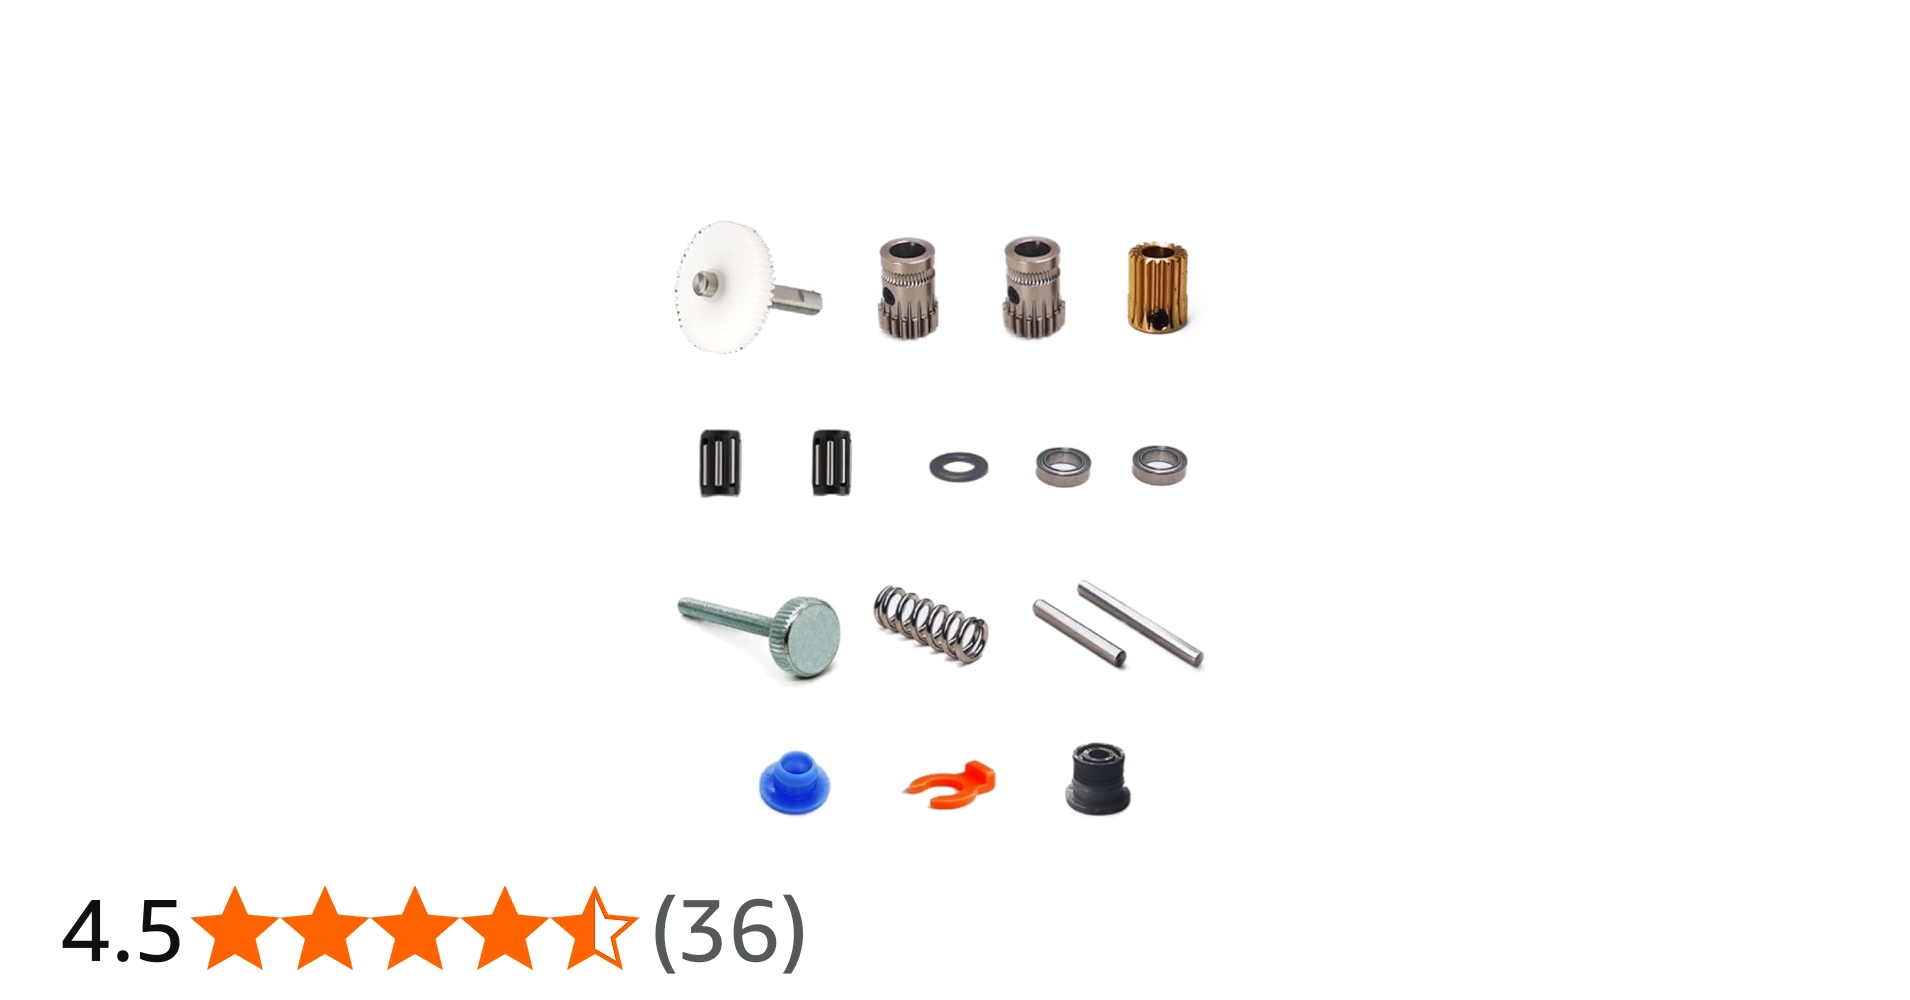
3D Printer BMG Accessories Reduction Mechanism AB extruder GEA kit for Voron V0.1/1.8/2.4
knotty gazelle
zealous cargo
Thought that was the difference?
Yes, that is the diffrence, Sherpa and Wristwatch does it to shrink the footprint. I just thought you may be confusing names, because IDGA is specific Bondtexch product and not BMG drive gear position.
zealous cargo
I switched from the idga WBMG to the "standard" one and flipped the gears
knotty gazelle
zealous cargo
I switched from the idga WBMG to the "standard" one and flipped the gears
I believe there's also mod for SB version of gears
Mod for WWBMG that is
I swear I saw it somewhere
near orchid
zealous cargo
I printed a different one with the same settings and it didn't do this
mine moves like this. there should be some axial movement
when you insert the filament, it constrains the axial movement
you kinda want it to move back and forth because it allows the gears to self-align
near orchid
especially on WW BMG because the set screw is not accessible when filament is loaded, so you cannot adjust the position of the gear
 analog hound
Yo guys, can someone help design a custom adapter mount for the Dragon Burner?
I own a Kobra 2 and I wanna mod the hell out of that thing, just for fun and learning, and I was thinking of changing the stock toolhead with the Dragon Burner. But I can't figure out which holes are used for mounting the toolhead on a mount; I obviously looked at the CAD but I'm simply too dumb.
Can someone give me some advice? Thank you!
native rapids
We can’t provide support for non voron printers. You will have to seek advice from whichever communities exist for your machine.
analog hound
my bad, I didn't mean to ask for support on a non-Voron printer
I just need a quick clarification on the Dragon Burner design itself: which exact holes on the toolhead body are meant to attach it to a mount? I'm designing my own custom cowl/mount from scratch and just need to know which standard mounting points to reference in the CAD.
ruby pumice
analog hound
my bad, I didn't mean to ask for support on a non-Voron printer
I just need a qu...
Maybe ask in #1182811180566331432
analog hound
ruby pumice
Maybe ask in <#1182811180566331432>
Thank you
 wide lodge
@potent python it looks like a good cleaning didn't do it either. I think I just have a bad set of gears
 wide lodge
 potent python
wide lodge
<@195286997240250368> it looks like a good cleaning didn't do it either. I think...
Hmmm, this sawtoothy kinda thing over the top of that photo honestly makes me wonder if theres something else afoot. Got a klipper.log you can share?
wide lodge
wide lodge
potent python
Hmmm, this sawtoothy kinda thing over the top of that photo honestly makes me wo...
It's a few days old but I've been having this problem for a bit.
potent python
wide lodge
Hmmm, might be worth trying stealthchop off on the z motors for a print.
I assume the mihai test was vase mode so z hop wont be an issue.
wide lodge
Actually I did 2 perimeters
potent python
Oh, thats destroyed its meaning
That may explain some confusion of mine.
Vase mode is necessary, it forces a repetition in a decreasing pattern. Shows up extruder vs motion clearly that way
wide lodge
Ok I'll try vase mode in the morning.
wide lodge
potent python
Vase mode is necessary, it forces a repetition in a decreasing pattern. Shows up...
This is in Vase mode. I also turned stealthchop on my z motors off
 wide lodge
 potent python
wide lodge
Ive just noticed extruder is also on stealthchop :D. I was looking to check the current. Ive seen before with low current some weird artifacts like the tiny wiggles you have in places. Your current looks good where it is, but im totally unsure if stealthchop could cause it tbh.
Does this look better in person, or are photos misleading?
wide lodge
potent python
Ive just noticed extruder is also on stealthchop :D. I was looking to check the ...
The photo is misleading. the single layer just had too much cooling and it rippled a bit
my current is set to 0.65A
actually extruder is not in stealthchop mode. I have TMC Autotune set to performance
potent python
wide lodge
actually extruder is not in stealthchop mode. I have TMC Autotune set to perform...
Well that answers that. Im guessing autotune also changes current, do you know what it sets it to?
Im also not seeing this stuff in your log file.
https://github.com/andrewmcgr/klipper_tmc_autotune#how-do-i-know-tuning-was-applied
But your log looks like its from before klipper has finished booting, so maybe it just didnt get around to that yet.
GitHub
TMC stepper driver autotuning Klipper python extra - andrewmcgr/klipper_tmc_autotune
wide lodge
potent python
Well that answers that. Im guessing autotune also changes current, do you know w...
Here is one I just did. TMC Autotune should touch the current.
potent python
Thanks. Yeah, all the stuff you said seems correct.
Hmmm.
Only easy thing i havent mentioned, when you drop the motor gear into tje extruder, it should go in easy. No fighting at all, and have a little play. But i dont suspect youd have gotten that wrong.
wide lodge
Ya I 've made sure it sit in smoothly. I did notice I didn't have much back and forth play and made a modified back plate that didn't change anything so I went back to the original. I do notice some defects in the injected molded parts but I didn't see anything around the teeth and it looks cosmetic but that my only other theory.
potent python
Starting work now, back later.
potent python
Yeah im a little lost for theories tbh. If you navigate to my github (through my bio) you can use this test print to take some measurements and fill out a spreassheet. Hopefully thatll give me some numbers something close to the lgx lite stuff, and i might get an idea of where that small scale wave pattern is being produced.
wide lodge
potent python
Yeah im a little lost for theories tbh. If you navigate to my github (through my...
This is pattern 1 the large wood grain pattern
 potent python
wide lodge
This is pattern 1 the large wood grain pattern
Any chance you could annotate one of those photos to show me pattern 1 and 2?
wide lodge
and here is pattern 2 the sawtooth pattern
 wide lodge
potent python
Any chance you could annotate one of those photos to show me pattern 1 and 2?
Here's the photos of the print. I edited to make the lines pop. The sawtooth goes all the way up and down the model

 potent python
wide lodge
Here's the photos of the print. I edited to make the lines pop. The sawtooth goe...
The larger one definately feels like something mechanical. Hobbed teeth tend to have similar spacing reguardless of gear. These g2 gears are made by bondtech, so stands to reason the spacing would be similar to lgx or bmg. So it could still be that. The smaller, fast repeating pattern. That one honestly could be that the motor is unhappy with something. That might be something that never goes away, or goes away very quickly when you ask for a higher flow rate or different run current.
I cant be sure either way if its hobbed teeth (so just tension), or some set of interactions in the planetary gearbox from the numbers, but they are helpful in saying that larger grain is absolutely mechanical, and absolutely extruder. Playing with autotune on/off, and different run currents between 0.5 and 0.65 might get a better result on the small one. Unfortunately thats about all the help i can give you. Its a real shame as g2 has been beautiful for me and youd absolutely want better results.
wide lodge
potent python
I cant be sure either way if its hobbed teeth (so just tension), or some set of ...
maybe I should just switch over to WWBMG. I have a 10T moons motor and all I would need is the RIGDA. It would also help with my Crazy Ivan setup.
potent python
wide lodge
maybe I should just switch over to WWBMG. I have a 10T moons motor and all I wou...
It seems the easiest option. Would be kinda sad, but maybe on another machine, with another stepper driver or something, it mysteriously behaves better.
wide lodge
potent python
It seems the easiest option. Would be kinda sad, but maybe on another machine, w...
I have gone through the driver settings and tried many different things. current, stealthchop, toff, coolstep etc. I think one thing is probably defective and I'm just not sure which part. I may have had these same issues with my stealthburner and G2E but I had other issues because I'm running a dragon uhf mini.
wide lodge
Already printed the new extruder
wide lodge
My gosh... this thing is tiny
wide lodge
Is this offset normal for the moonS 10T motor and RIDGA?
 wide lodge
 pine sun
Yes 🙂
Thanks. I guess I'll try and make a fix.
pine sun
wide lodge
Thanks. I guess I'll try and make a fix.
Theres not really much more space because the bearing or shaft of the 50t gear is already almost touching the motor
wide lodge
pine sun
Theres not really much more space because the bearing or shaft of the 50t gear i...
I'm seeing like 1-1.5mm of gap from the end of the shaft to the back of the plate when I align the RIDGA with a piece of filament.
pine sun
My memory might be wrong then 😄
wide lodge
pine sun
My memory might be wrong then 😄
 wide lodge
I did remember reading the back shaft was 3mm and I'm measuring 2.5mm which matches the bearing
wide lodge
Well that's about as good as it's going to get


 rough topaz
void sequoia
Hi all, is there a specific good go-to for HGX 2.0 gears? I’ve had a couple of ...
Which extruder is this?
void sequoia
rough topaz
Which extruder is this?
My own design. Haven’t named it yet.
rough topaz
void sequoia
My own design. Haven’t named it yet.
Ahhh, so I can assume unreleased then?
void sequoia
rough topaz
Ahhh, so I can assume unreleased then?
Yep. I’d like to release it but I still haven’t found a reliable source for good gears.
native rapids
void sequoia
Yep. I’d like to release it but I still haven’t found a reliable source for good...
what have you tried so far?
void sequoia
The first set I got that was good I got on AliExpress and then couldn’t find it again. I got another set on Ali and a couple on Amazon and they were a little out of concentricity. They work well enough but I suspect I’m getting some inconsistent flow on tools 2 and 3 on my Stealthchanger.
native rapids
have you tried proper bondtech gears yet?
void sequoia
Yes, on my previous design. They’re thicker than the HGX2.0 gears so they wouldn’t fit on this version. I have considered giving up and just going back to the LGX gears.
pine sun
wide lodge
Well that's about as good as it's going to get
That's actually pretty nice!
I should look into my setup how it looks there, tho I never had problems with it. There is used ridga v2 gears aswell
wide lodge
pine sun
That's actually pretty nice!
I should look into my setup how it looks there, tho...
I need to move it a smidge back for filament alignment but gear tooth engagement should stay at about 95%. The only way to get full engagement would be to have the bearing and maybe shaft against the motor. Once I'm finished, I can upload it if you want to try it.
rough topaz
wide lodge
Here's the photos of the print. I edited to make the lines pop. The sawtooth goe...
I see you were testing wood grain and building a RIDG extruder... what was thew result of your testing. Was the RIDGA an improvement? What did youy start with?
wide lodge
rough topaz
I see you were testing wood grain and building a RIDG extruder... what was thew ...
I'm still making adjustments to the WWBMG to fit the RIDGA better. I think this is the last adjustment I will need.
What you see in the test here show exactly what I started with. Nothing I did to my WWG2 helped the wood grain.
wide lodge
I might have to wait for a new motor... Black wire insulation is coming up right at the base
 wide lodge
But the engagement is great, doesn't touch the motor. There is probably at least a 10mm difference between this and the WWG2 comparing where the back of the motor sits
 rough topaz
wide lodge
What you see in the test here show exactly what I started with. Nothing I did t...
Even a smooth (bearing?) idler?
Its so funny...Ive chased wood grain through a few gear sets. have found 2 cheap BMG gears that just work flawlessly in a CW2, whether its the luck of alignment as they sit, or the luck of the gear cut not producing wood. I wonder if more precisly cut gears gaurentee woodgrain. At least with poorly cut gears you might get lucky some how.
ruby pumice
wide lodge
I might have to wait for a new motor... Black wire insulation is coming up right...
If the motor is working, you could try to DIY a strain relief for it. Maybe E6000 which is flexible but strong
Makes me want to put E6000 on mine before install
wide lodge
ruby pumice
If the motor is working, you could try to DIY a strain relief for it. Maybe E60...
Well I have some left over RTV that might work
wide lodge
rough topaz
Even a smooth (bearing?) idler?
Heck ya! I'm not leaving it up to chance. Might use my G2 tensioner screw because the BMG is super tight
rough topaz
wide lodge
Heck ya! I'm not leaving it up to chance. Might use my G2 tensioner screw becaus...
Wait, you are infact getting bad woodgrain with a smooth idler?
wide lodge
rough topaz
Wait, you are infact getting bad woodgrain with a smooth idler?
I was getting wood grain on my G2 with a smooth idler. No idea why
wide lodge
ok I do have it on and started testing. That smooth idler arm adds a of pressure. might need to be modified if its too high.
wide lodge
Well, it can do at least 50mm³/s
rough topaz
wide lodge
I was getting wood grain on my G2 with a smooth idler. No idea why
Ha, and its a rigda bondtect gear set yeah?
wide lodge
rough topaz
Ha, and its a rigda bondtect gear set yeah?
no that was the Galileo 2 gears
 buoyant wind
wide lodge
I was getting wood grain on my G2 with a smooth idler. No idea why
Strange how periodic is it. Might possibly be that the pinion isn’t perfectly aligned with the spider shaft and planets
wide lodge
buoyant wind
Strange how periodic is it. Might possibly be that the pinion isn’t perfectly al...
What's even stranger is it may have somehow not been the extruder.
@potent python hey I just swapped extruders and it seems that sawtooth pattern is still there


 wide lodge
I think the wood grain is still there but it is harder to see
potent python
The sawtoothing is cooling related.
the stuff at the corner that is
Or PA maybe i guess. Dirty nozzle even.
But thats a print designed to make obviously visible patterns if theres an extruder problem. If you're not able to see that on this print, youll never see it on any other.
potent python
rough topaz
Wait, you are infact getting bad woodgrain with a smooth idler?
Woodgrain has always been caused by a poor mesh between the motor and 50t gear in my experience.
With the vanishingly few exceptions of it being caused by motor resonance.
And never seen anyone not fix it, and have to change to a smooth idler.
 tepid sierra
New v02 build here with the miniSB. I'm getting intermittent under extrusion that presents itself a bit like heat creep, but it's right out of the gate when I start printing. I'll get maybe 10 seconds of solid extrusion, and 5 of just sporadic blobs, then a period of proper extrusion, then sporadic blobs. It happens with PLA, ABS, PETG - all straight out of my dry box at 10% humidity. All parts printed quite nicely (way nicer than the parts that went into the 2.4 that birthed this 0.2) and the toolhead went together quite well. I only needed to sand the shaft of the gear down to fit into the bearings. It's still just a little tiny bit snug - it slips in without force, but doesn't slide freely. Could this be my issue? edit: Teeth marks are visible on clear PLA, but can only see them in the reflection on my lighter colored filaments. I'm not getting any clicking sounds from the stepper.


 tepid sierra
Thank you so much. I could have just looked at the filament on my other printer, but didn't because I an idiot. 🙂
Increasing spring tension significantly didn't improve anything, likely the antiquish thinger is adjusted out too much?
tepid sierra
potent python
https://cdn.discordapp.com/attachments/921882154990989333/1165372068892770364/PX...
Anti-squish thinger! Such a simple fix, I just got caught on all the other problems it could be. Thanks!
wide lodge
potent python
But thats a print designed to make obviously visible patterns if theres an extru...
Well the problem I have have is it shows up as vertical lines that look like ringing even on thicker prints.
Admittedly it's not fully calibrated. Mostly just wanted to see if the same pattern was there and it unfortunately is.
 twilit orchid
for the orbiter, is there a replacement for the steel filament exit guide ? Just print it ?
rough topaz
wide lodge
Admittedly it's not fully calibrated. Mostly just wanted to see if the same patt...
All kind of issues acn arise from over extrusion. If you havent tuned your EM, start there. Try loweing the EM past op6timal a few % and try again... Just saying in case you havent already.
 iron cosmos
In 2026 is there a go to extruder? I had an orbiter 2.5 on my ender, was debating buying another or going wwg2
native rapids
iron cosmos
In 2026 is there a go to extruder? I had an orbiter 2.5 on my ender, was debatin...
i have a soft spot for galileo stuff, but orbiter is good too. g2 obviously has the fun of printing/building with it
iron cosmos
native rapids
i have a soft spot for galileo stuff, but orbiter is good too. g2 obviously has ...
That was my sticking point lol. As long as there's not a huge winner then I'll keep thinking about it
deft galleon
iron cosmos
In 2026 is there a go to extruder? I had an orbiter 2.5 on my ender, was debatin...
I'm a planetary gear fan for extruders and I'm an Orbiter fan, so I can easily recommend them. I do have kits for the G2E but my Obiter and Orbiter derived extruders just keep on working
iron cosmos
deft galleon
I'm a planetary gear fan for extruders and I'm an Orbiter fan, so I can easily r...
I do like just keep working. As long as both are still good (and it sounds like trhy are). I wanted to check cause a lot of posts ive seen on it were old
wide lodge
rough topaz
All kind of issues acn arise from over extrusion. If you havent tuned your EM, s...
So I did optimize and it didn't really change. I think now despite the wood grain pattern, it's not the extruder.
potent python
twilit orchid
for the orbiter, is there a replacement for the steel filament exit guide ? Just...
Cut some PTFE tube to fit as best you can?
Might wanna make sure it wedges in there to stop it spinning at hitting the gears. A layer of electrical tape does okay with that in printed parts
hybrid fog
twilit orchid
for the orbiter, is there a replacement for the steel filament exit guide ? Just...
Hey man pick a flag in #rules because I’m your near me I may have a part for you. (Victoria Australia 🇦🇺)
 keen moth
hybrid fog
Hey man pick a flag in <#869236671554682990> because I’m your near me I may have...
Tassie
hybrid fog
keen moth
Tassie
so i have a o2.5 collecting dust if you where nearer to me i would swap it lol
keen moth
Thanks mate, it would cost more to make the journey than to buy a new one, or ten 😂
 marsh fractal
Did I screw something up or is the the amount of gear engagment for a WWBMG with RIDGA?

Seems like there should be more overlap between the stepper and RIDGA
 rugged yew
On WW-IDGA I'm running into and issue with the tension arm, my first issue was the pin backing out and the dual drive gear losing tension, now the main screw holding the pivot backed out and I lost tension, I think I solved the pin issue but would some lock tight be the answer for the pivot screw

 warm hare
Working on a WWBMG ridga for the A4T, and I feel like the main shaft of my gear set is slightly too long, requiring the motor plate to have to bend around the rear bearing


I reprinted the parts scaled up 100.6% to remove any shrinkage but still having the issue
warm hare
I think the small shoulder on the rear side of the main gear is the issue, this set is from aliexpress and it looks like the gear is supposed to be ~ 1 mm to the left, which would clear space up
 wide lodge
marsh fractal
Did I screw something up or is the the amount of gear engagment for a WWBMG with...
No this is normal. Had the same issue with my moons 10T. I actually modified a plate to get more engagement.
wide lodge
warm hare
I think the small shoulder on the rear side of the main gear is the issue, this ...
It's probably too far off the Bondtech spec. The shaft is probably rubbing on the motor
iron cosmos
Any issues with the mellow orbiter 2.5 vs the triangle labs? Looks like it's on sale for 45
I'm between a wwbmg, sherpa mini or orbiter
Or ww g2...
Leaning ww g2 but I like the idea of just getting a fully built orbiter/sherpa
wintry dew
I like my WWG2 but I think those are cheaper from West3D /Fabreeko/KB-3D than getting them on AliExpress.
iron cosmos
wintry dew
I like my WWG2 but I think those are cheaper from West3D /Fabreeko/KB-3D than ge...
The wwg2 does seem very popular
iron cosmos
Kinda leaning sherpa cause it looks cool...
warm hare
I have a sherpa in use right now, only ~150 hours on it but its been very reliable
The thing I don't like is I feel like there are more/better thought out toolhead boards for WWMBG, at least for the nitehawk36
iron cosmos
warm hare
The thing I don't like is I feel like there are more/better thought out toolhead...
Not sure what you mean
iron cosmos
Aren't toolhead boards mainly just based on a circle or square motor?
ruby pumice
You could say that, except for the ones designed for SB.
But you could also just say they are all designed for the pancake since the last common square one was CW1
deft galleon
iron cosmos
Any issues with the mellow orbiter 2.5 vs the triangle labs? Looks like it's on ...
AFAIK, they're the same extruder from LDO
I'm also a planetary gear fan with extruders and use the Orbiter v2 (and derived extruders) on my printers
iron cosmos
deft galleon
I'm also a planetary gear fan with extruders and use the Orbiter v2 (and derived...
Didn't realize there's derived extrudera from an orbiter. That's cool then
ruby pumice
Yeah, the interesting dilemma becomes which you like more - O2 or G2. I run both
iron cosmos
ruby pumice
Yeah, the interesting dilemma becomes which you like more - O2 or G2. I run both
Do you just take apart the orbiter and move the gears over?
deft galleon
iron cosmos
Do you just take apart the orbiter and move the gears over?
They won't fit the G2, although I think someone may have done a version of the G2 to use the gubbins from the Orbiter v2.* but I know no more about that. The G2 kit is quite a bit different to the Orbiter v2
native rapids
i have seen at least one attempt to self produce an orbiter from the rough CAD robert offers for it
ruby pumice
iron cosmos
Do you just take apart the orbiter and move the gears over?
Yeah its not that kind of situation, you have to pick in advance. The G2 kit can be built into a bunch of different printed extruder setups tho
iron cosmos
ruby pumice
Yeah its not that kind of situation, you have to pick in advance. The G2 kit ca...
That's more what I thought. I didn't realize people use the orbiter for anything else.
I have an orbiter and ebb36 Gen 1 in my ali cart atm... Just deciding if i want to pull the trigger lol
 glad locust
I’m having some major issues with my CW2, randomly out of nowhere it started chattering and making noises. Klipper then throws a warning that my ebb thermistor is close to 100c, so I shut down the printer. When I touch the stepper it is well over 100 degrees. I’ve let everything cool down and I’ve reassembled the tool head. It still makes a smaller chattering noise and refuses to extrude. I also have filament stuck in my hotend now, fully stuck. Will not move from either end
I have 2 of the same beam 14 stepper coming tomorrow for a different build, will try swapping the motor and see if that changes anything. It might just be burned out
knotty gazelle
what's yout run_current on that stepper motor and what is the motor rated for?
It's usually way lower than what the label says
glad locust
It’s rated for 1 amp, and I was running it at 0.71. However looking into my config files I found that my gear ratio was 50/17, I think this may have caused some issues. I don’t know why they presented themselves now though, the printer was running fine for 80 hours, and the print it stopped on wasn’t a long one
glad locust
looks like it may just have been a nasty hotend clog, steppers got delayed so I'm gonna run some tests with the one that "overheated"
knotty gazelle
glad locust
It’s rated for 1 amp, and I was running it at 0.71. However looking into my conf...
0.71 sounds a lot, people usually run up to like 0.6.
Gear ratio for CW2 is 50:10 if your stepper motor has 10 🦷
glad locust
The extruder works, but I’m getting a strange artifact in corners. I made sure to recalibrate my rotation distance
 glad locust
knotty gazelle
0.71 sounds a lot, people usually run up to like 0.6.
Gear ratio for CW2 is 50:1...
I double checked and manually counted everything, it’s 50:10
knotty gazelle
Those little motors get very hot, I'd start at like 0.4 and if it does not keep up, then increase.
knotty gazelle
glad locust
The extruder works, but I’m getting a strange artifact in corners. I made sure t...
That looks like pressure advance?
Do you have any PA in your config?
glad locust
Not in firmware no. everything is done in orca
knotty gazelle
You did not put any PA values in your Klipper?
glad locust
Nope, didn't alter anything in the config aside from rotation distance, gear ratio and run current
I'll run a recalibration just for safety's sake
The recalibration is not looking good….
I don’t think that’s what it’s supposed to look like
 knotty gazelle
glad locust
I don’t think that’s what it’s supposed to look like
No.
Just in case double-check you pressure advance value in config itself?
glad locust
No config Pressure advance, only through slicer. Trying a fresh slicer profile cause the old one was calibrated for the incorrect extruder settings
rugged yew
running WWidga and a pika. my max flowrate caps out around 25 when my extruder motor start skipping steps. is this something that can be solved by upping the stepper current, i currently have run_current: 0.65 stealthchop_threshold: 0
previously on cw2 with ebb sb the gears would skip, but with the ww and ebb36 gen2 the stepper skips
mellow cradle
what filament / print temperature?
rugged yew
pla at 220
going hotter doesnt seem to help
petg at 255 caps out at 20mm^3/s
i dont have to go faster, i just bought the whole pika so kinda want to use as much as possible
mellow cradle
sure, just making sure you had considered hotter like 230 for pla for example