

1 messages · Page 1 of 1 (latest)
 dense geode
Printing on an ender 5 pro with PLA. Using cura slicer with standard settings, is the issue of weak supports a setting such as line thickness I should change? Also is the stringing something I can fix with retraction or does it not really matter?
 dusky lichenBOT
dense geode
Printing on an ender 5 pro with PLA. Using cura slicer with standard settings, i...
For weak supports, you can try increasing the support density or infill percentage in your slicer settings. Adjusting the line thickness may help in some cases, but support density is usually more effective.
Stringing can often be improved by adjusting retraction settings in your slicer. Increasing retraction distance and speed can reduce stringing. It's also worth ensuring your filament is of good quality and your hotend temperature is properly calibrated.
dense geode
Printer is ender 5 pro, filament is hatchbox pla white, the slicer is cura, I have changed settings to increase flow rate, enabled z hop with retraction, and increased wall count to 3 instead of 2.
 lusty heart
For your stringing...
I'd be checking if your filament is wet....
If not, then retraction 👌
dense geode
lusty heart
For your stringing...
I'd be checking if your filament is wet....
If not, then r...
I just had it in a dehydrator for about 9 hours and its still the same, should I increase or decrease the retraction to fix it?
lusty heart
dense geode
I just had it in a dehydrator for about 9 hours and its still the same, should I...
Oo ok.
Increase retraction distance or retraction speed...
In small increments til you get something thats better...
https://www.3dsourced.com/rigid-ink/ultimate-3d-printing-troubleshooting-guide/#stringing-oozing
https://ellis3dp.com/Print-Tuning-Guide/articles/retraction.html

You’re here because you’ve either just had a complete 3D print failure, or your prints aren’t quite perfect. We don’t settle for less than perfect, so we
dense geode
lusty heart
Oo ok.
Increase retraction distance or retraction speed...
In small increments ...
I just tried it and the issue is still there
Sorry, I think I worded it wrong
The issue is the print itself is stringy
Like in places where it's just making a line none of them are sticking to the previous one and are becoming stringy
lusty heart
dense geode
Like in places where it's just making a line none of them are sticking to the pr...
Ok so i'll get you to check whether the filament is tensioned properly....
If you have a nozzle needle, i'd try giving the nozzle a clean too...
Heres some more comprehensive info on what it could be.
https://www.3dsourced.com/rigid-ink/under-extrusion-problems-clicking-sounds/
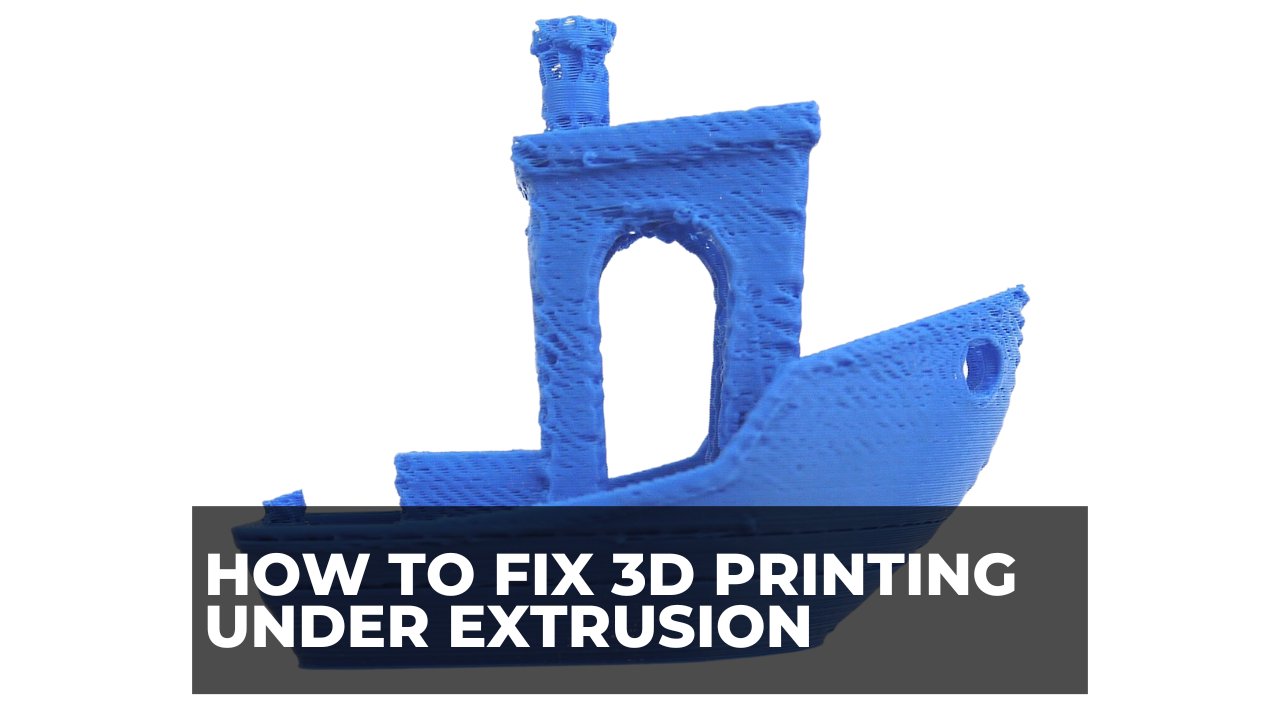
Under-extrusion in 3D printing occurs when the printer's nozzle can't dispense enough filament, leading to incomplete or weak prints.
dense geode
I tried cleaning the nozzle and it felt like something that was stuck got pushed out when I put the needle in
I'll try swapping it out and see if that fixes it
dusky lichenBOT
This post has been inactive for over 1 hour and so has been closed. To reopen this post simply send another message.
dense geode
lusty heart
Ok so i'll get you to check whether the filament is tensioned properly....
Swapped to a new nozzle, cold pulled the nozzle 6 times until there wasn't anything visible in the filament, trimmed the bowden tube to a fresh part, and it's still coming out spongy/stringy
It matches up with the under extrusion/clog issue but I'm not sure what else I can do
Just printed this as a test, it's supposed to be a solid cylinder
 dense geode
I changed the flow to 140%, speed from 80 to 60 mm/s, and temp to 220°C
It's printing like this now but there's still small areas where it looks deformed and the inside layers aren't sticking together

 dense geode
I've narrowed it down to the extruder
I set it to extrude 100mm and it only pushes out 40mm
lusty heart
Ooh ok...good job!
Look for a guide on calibrating your extruder e-steps....and then that should make it match up...
dense geode
Just finished calibrating the e-steps and test print came out great.
I had to change it from 93 to 234 which seems like a big jump, I wonder if the stepper was somehow damaged since it wasn't a gradual change in the print quality.
dusky lichenBOT
Is your problem solved? / No longer need this channel?
You can close a help channel with ?solved when it is no longer needed.
