#Filament clustering on nozzle
1 messages · Page 1 of 1 (latest)
 cerulean dagger
 kind impBOT
cerulean dagger
It is leveled, and everything. I just changed the speed in orcaslicer. Maybe its...
AI Help
It sounds like the issue you are experiencing could be related to the extrusion speed setting in OrcaSlicer. Try checking the extrusion multiplier or flow rate settings to ensure that the filament is being extruded at the correct speed. You may need to adjust these settings to increase the extrusion rate if the print is coming out too slowly. Additionally, make sure that the nozzle is not clogged and the filament is loaded properly. If the issue persists, you may need to further troubleshoot the extruder mechanism itself.
WARNING: This response is AI generated and may contain errors.
 kind impBOT
cerulean dagger
https://www.wevolver.com/article/z-offset-what-it-is-and-how-to-adjust-it
TLDR:
Setting your z-offset correctly ensures a good first layer squish and proper adhesion to the build plate (assuming its clean, see
?bedcleaning for more information). See
?leveling for a good representation of how the first layer should look like.
If in doubt: Refer to you your specific machines documentation.
For the Qidi X series printers: Adjusting the z offset from the Fluidd webinterface breaks it. Always set the z offset from the printers screen.
?z-offset requested by: m.von.d#0
 chilly coral
You compared all settings?
cerulean dagger
chilly coral
You compared all settings?
well the only difference is orcaslicer speed settings are faster than flashprint slightly
everything else is the same i think but im new to orcaslicer
chilly coral
cerulean dagger
well the only difference is orcaslicer speed settings are faster than flashprint...
Then turn them down for the first layer at least. The picture looks like its not adhering at all though
cerulean dagger
chilly coral
Then turn them down for the first layer at least. The picture looks like its not...
first layer is default
 chilly coral
Thats slow
cerulean dagger
chilly coral
Thats slow
Look how thin it's extruding

it needs to be way thicker than that, so it wont stick to the plate
chilly coral
cerulean dagger
Look how thin it's extruding
Looks like the nozzle is too close
cerulean dagger
chilly coral
Looks like the nozzle is too close
i tried moving it closer and further
just caused more problems
chilly coral
cerulean dagger
i tried moving it closer and further
Interesting
cerulean dagger
adventurer 3 problems
cerulean dagger
chilly coral
Interesting
but still, flashprint works fine with it
first layer is the same as flashprint settings
chilly coral
Yeah sounds like it. Got the start gcode set up the same?
cerulean dagger
chilly coral
Yeah sounds like it. Got the start gcode set up the same?
uhhh
i dont think flashprint gives you that info
yeah it doesnt
cerulean dagger
chilly coral
Yeah sounds like it. Got the start gcode set up the same?
any idea?
been trying this bs since 8am
chilly coral
Flashforge are the worst
cerulean dagger
now its 10:44
cerulean dagger
chilly coral
Flashforge are the worst
agreed, im gonna buy qidi q1 pro soon
but its gonna be a while bc $500
hoping it doesnt get out of stock on amazon 😭
chilly coral
Theres apparently a way to read the .gx files that flashprint spits out. You could try getting the start gcode from there
cerulean dagger
chilly coral
Theres apparently a way to read the .gx files that flashprint spits out. You cou...
if youre able to extract it, 🤷♂️
maybe i have the wrong one set?
 chilly coral
;machine_type: Adventurer 3 Series
;right_extruder_material: PLA
;right_extruder_material_density: 1.24
;filament_diameter0: 1.75
;right_extruder_temperature: 210
;layer_height: 0.18
;perimeter_shells: 2
;top_solid_layers: 4
;bottom_solid_layers: 3
;fill_density: 15%
;fill_pattern: hexagon
;base_print_speed: 60
;travel_speed: 80
;platform_temperature: 50
;right_extruder_temperature_raft0: 215
;right_extruder_temperature_reset:
;left_extruder_temperature_reset:
;layer_total_count: 449
;start gcode
M118 X26.94 Y52.60 Z81.65 T0
M140 S50 T0
M104 S215 T0
M104 S0 T1
M107
M900 K0.000 T0
G90
G28
M132 X Y Z A B
G1 Z50.000 F420
G161 X Y F3300
M7 T0
M6 T0
M651 S255
;layer_count: 449
M108 T0
G1 X-26.60 Y21.78 F4800
;preExtrude:0.20
M106
G1 Z0.200 F420
;structure:pre-extrude
G1 X-26.60 Y21.78 F4800
G1 X-26.60 Y-46.11 E9.8450 F1200
G1 X-26.35 Y-47.85 E10.0999
G1 X-25.58 Y-49.55 E10.3706
G1 X-24.37 Y-50.97 E10.6411
G1 X-22.81 Y-51.99 E10.9114
G1 X-21.07 Y-52.52 E11.1752
G1 X-20.06 Y-52.60 E11.3221
G1 X20.11 Y-52.60 E17.1473
G1 X21.85 Y-52.35 E17.4022
;raft
;layer:0.40
;support-start
G1 E12.4022 F1500```Well
Just rename as .txt
cerulean dagger
chilly coral
```gcode_flavor: flashforge
;machine_type: Adventurer 3 Series
;right_extruder_m...
i dont understand this
at all 🤣
chilly coral
Just compare the start gcode sections or better yet post the orcaslicer one
cerulean dagger
chilly coral
Just compare the start gcode sections or better yet post the orcaslicer one
M140 S[bed_temperature_initial_layer] T0
M104 S[nozzle_temperature_initial_layer] T0
M104 S0 T1
M107
M900 K[pressure_advance] T0
G90
G28
M132 X Y Z A B
G1 Z50.000 F420
G161 X Y F3300
M7 T0
M6 T0
M651 S255
end g code:
M104 S0 T0
M140 S0 T0
G162 Z F1800
G28 X Y
M132 X Y A B
M652
G91
M18
seems very different. another part is that theres no 'flashforge' in gcode flavor section on orcaslicer
cerulean dagger
cerulean dagger
maybe i have the wrong one set?
only these
chilly coral
yeah that should not matter
cerulean dagger
chilly coral
yeah that should not matter
so any idea
chilly coral
Not really, sorry.
cerulean dagger
damn
cerulean dagger
chilly coral
Not really, sorry.
well imma try to set the flow rate / extrusion speed
man wth is this
 chilly coral
I would try the tried and true trifecta of bedcleaning, releveling, zoffset
cerulean dagger
chilly coral
I would try the tried and true trifecta of bedcleaning, releveling, zoffset
i did alr
cerulean dagger
chilly coral
The factor of the flow
where is extrusion speed then
aka how fast it pushes out filament
etc
chilly coral
That is the exteusion speed
Its the factor to calculate how much filament is transported how fast
cerulean dagger
chilly coral
Its the factor to calculate how much filament is transported how fast
what is 25mm/s then

what would that be on orcaslicer
chilly coral
speed at which the filament is pushed after a retraction
cerulean dagger
how do i calculate
chilly coral
cerulean dagger
how do i calculate
You don't, you tune with a retraction tower. 99% the default is fine
cerulean dagger
chilly coral
You don't, you tune with a retraction tower. 99% the default is fine
Ight I'm just gonna sell this printer
Make some money off of it 💀
cerulean dagger
chilly coral
You don't, you tune with a retraction tower. 99% the default is fine
This is what happens when I print with flashprint

Extrudes way more filament than orcaslicer
chilly coral
cerulean dagger
Extrudes way more filament than orcaslicer
You can try to increase the extrusion multiplier🤷
In orca
cerulean dagger
Alr
kind impBOT
This post has been closed due to inactivity.
This post has been inactive for over 1 hour and so has been closed. To reopen this post simply send another message.
cerulean dagger
chilly coral
You can try to increase the extrusion multiplier🤷
where is that?
i cant find it
?solve
kind impBOT
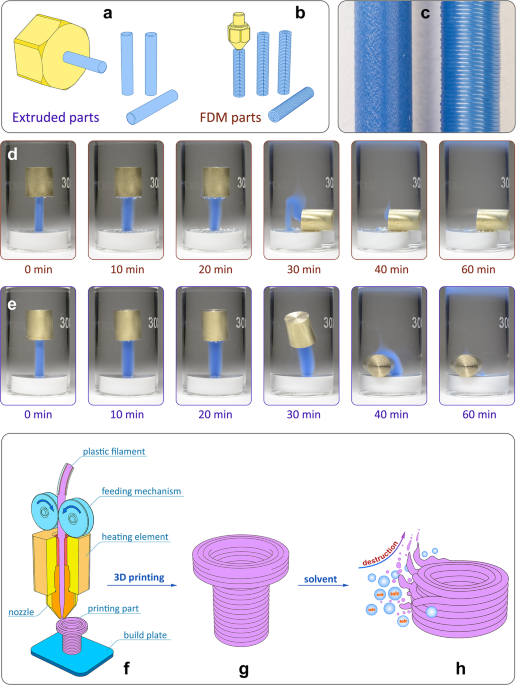
Nature
Scientific Reports - Revealing interactions of layered polymeric materials at solid-liquid interface for building solvent compatibility charts for 3D printing applications
kind impBOT
BenchyBot
BetaCommands:
add_printer Adds a printer to your name.
belt_freq Calculates target belt frequency (Hz) for correct tension base...
belt_tension Calculates the tension (N) in a GT belt based on the measured...
pi
random_thing Find a random thing from thingiverse.
time Used to get the current time in a timezone.
topic
GCode:
mg Used to search Marlin Gcode Commands.
HelpForum:
solved
No Category:
help Shows this message
Type ?help command for more info on a command.
You can also type ?help category for more info on a category.
?solved